Best Corrugated Pipe Machine for Your Production Needs
2026-10-20
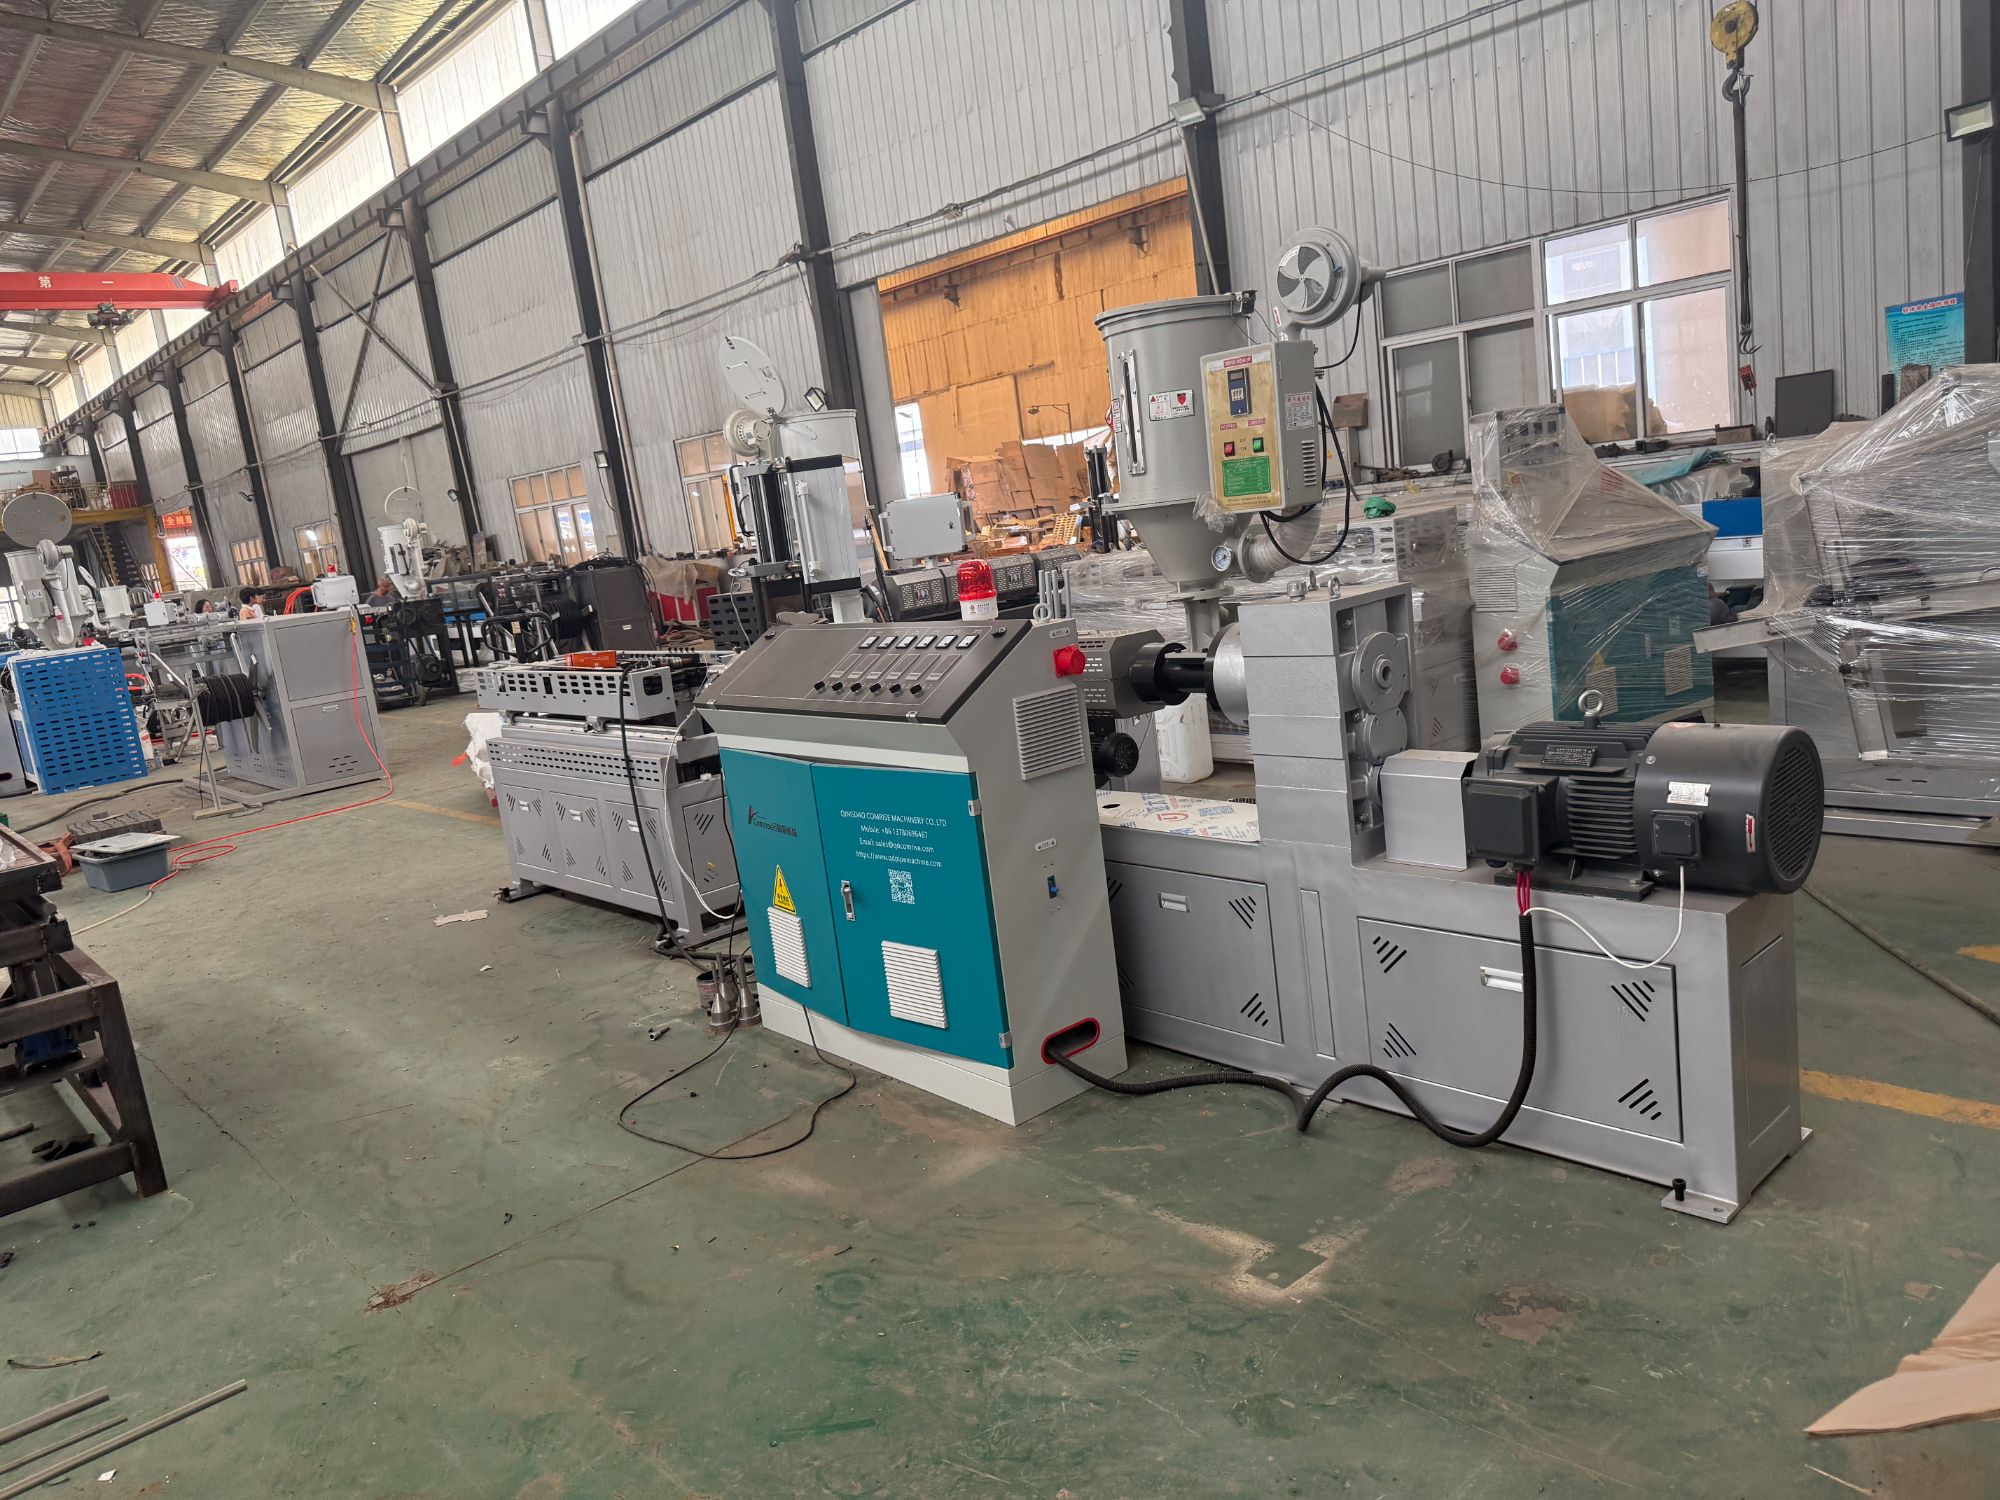
Choosing the right corrugated pipe machine isn't just about buying equipment—it's about securing consistent output, reducing downtime, and staying ahead of demand. Whether you're expanding a production line or replacing outdated machinery, the difference between a good machine and a great one shows up in every meter of pipe you produce. That's where COMRISE comes in. With a focus on precision engineering and real-world reliability, COMRISE has built a reputation for turning production challenges into measurable results. In this guide, we'll walk through what truly matters when selecting a corrugated pipe machine—and why hundreds of manufacturers trust COMRISE to keep their lines moving without compromise.
Matching the Machine to Your Material Mix
Selecting the right equipment rarely starts with horsepower or throughput charts. It begins with a clear picture of the materials actually moving through your line. A machine tuned for dense plastics will struggle when you introduce lightweight foams, and a system optimized for consistent shapes can stall when faced with mixed packaging waste. The most reliable setups are those built around the material mix you handle today, while leaving room for the shifts that will arrive next year.
Different material blends create different demands. Abrasive streams wear rotors faster, high-moisture loads invite clogging, and bulky items test infeed geometry. Rather than chasing a universal solution, look at the specific ratios you process. Test runs with your own material profiles expose weaknesses that spec sheets cannot. A machine that comfortably handles a 70/30 cardboard-to-film mix may choke at 50/50, so match the cutting chamber, screen size, and feed mechanism to the actual blend you will feed it.
Flexibility matters, but it must be engineered, not assumed. Adjustable screens, reversible cutters, and variable speed drives give operators room to adapt without swapping entire units. Asking suppliers for references from operations with similar material mixes reveals real-world behavior. The goal is not the most expensive machine, but one whose wear parts, power draw, and maintenance schedule align with the unique mix your facility generates week after week.
Why Output Speed Alone Won't Save You Money
Many teams chase faster output as if it’s a direct line to lower costs. But a machine that prints pages quickly or a service that returns results in seconds doesn’t automatically shrink your budget. The real expense often hides in what happens after that fast output lands: misprints need redoing, rushed code introduces bugs that take days to untangle, and rapid-fire responses can miss the mark so badly that you pay twice for the same task.
Speed also tends to create bottlenecks elsewhere. If one stage of your workflow sprints ahead while the next can’t keep up, you end up with queues, idle time, or half-finished work piling up. Those delays cost more than the seconds you saved upstream. Money leaks through rework, overprocessing, and the need for extra oversight that a more balanced pace would avoid.
What actually protects your budget is consistent, dependable output that fits the whole process—not just the headline number. A slightly slower tool that gets it right the first time, integrates cleanly with your existing systems, and doesn’t demand constant babysitting can save far more than the fastest option on paper. Judge value by total cost per completed, correct unit, not by how quickly a job starts.
The Hidden Cost of Frequent Die Changes
On paper, swapping a die looks like a routine task: unbolt the old tool, bolt in the new one, get back to running parts. But every changeover quietly eats into margins in ways that rarely show up on a standard cost sheet. Setup technicians wait while machines sit idle, operators adjust first-off parts, and quality teams chase dimensional drift caused by slight misalignments. These minutes accumulate into lost production hours that no one officially logs as downtime—yet they directly reduce the number of sellable units per shift.
Beyond the obvious time loss, frequent die changes accelerate wear on clamping systems, locator pins, and press beds. Each mounting and removal introduces tiny nicks, scratches, and deformation that slowly degrade alignment precision. Over weeks, this results in higher scrap rates, more rework, and occasional tool damage that demands expensive repairs or early replacement. The real cost isn't just the die itself—it's the gradual erosion of process stability that forces operators to make constant micro-adjustments, often without documenting the root cause.
Many manufacturers overlook the cognitive load on their teams. When changeovers happen multiple times a day, workers fall into a hurry-up-and-wait rhythm, leading to rushed installs, skipped torque checks, or forgotten lubrication points. These small oversights compound into unplanned stoppages and safety near-misses. The hidden cost, then, isn't a single line item—it's a slow bleed of efficiency, accuracy, and team focus that only becomes visible when you compare actual output against theoretical capacity over a month, not just a single shift.
How Smart Controls Cut Scrap Rates
Traditional scrap often comes from small parameter drifts that go unnoticed until a batch is already out of spec. Smart controls close that gap by watching critical process variables in real time and making micro-adjustments before defects can form. In injection molding, for instance, in-cavity sensors track pressure and temperature curves, and the controller tweaks injection speed or hold time whenever a slight deviation appears, keeping every part inside tolerance.
Beyond live correction, smart controls learn from accumulated runs. They link signature patterns to specific defects like warpage, sink marks, or dimensional drift, then shift parameters ahead of time rather than waiting for scrap to appear. This closed-loop behavior cuts down on trial runs and manual tweaks, which are common sources of variation on the shop floor.
In machining operations where tool wear gradually erodes precision, smart controls monitor spindle load and vibration to compensate for wear. They can nudge feed rates or offsets without stopping production, preventing parts from drifting out of specification. The result is a measurable drop in scrap rates across batches, achieved without constant human oversight.
What to Look for in a Long-Life Corrugator
A corrugator that runs for decades doesn't happen by accident. The first thing I check is the main frame and how the rolls are seated. Heavy, vibration-dampening side frames with machined bearing housings make a real difference once speeds climb. Flimsy frames might look fine on paper, but they'll fight you with misalignment and worn bearings after a few years of three-shift runs.
Beyond the frame, pay close attention to the glue unit and the corrugating rolls themselves. Rolls with consistent chrome plating and properly crowned profiles hold their flute shape longer, which means less edge crush loss over time. And don't ignore the little things: accessible grease points, sealed bearings where possible, and a control system that logs roll hours. If you can't easily see wear coming, you won't catch it before it eats into your board quality.
Finally, ask about how the machine handles thermal expansion. Long corrugators heat up in sections, and if the design doesn't allow the frames and rolls to expand freely, you'll get premature surface wear. Look for expansion joints or floating bearing arrangements, and make sure the operators actually use the maintenance schedule instead of treating it as a suggestion.
Real-World Throughput vs. Brochure Numbers
Manufacturers frequently cite throughput figures that come from controlled lab environments, where a single device transmits over a clean channel with minimal interference and no competing traffic. These numbers assume perfect conditions: short distances, ideal antenna orientation, low noise floors, and often a fixed modulation scheme locked at its highest rate. In practice, your office or home introduces a very different picture, with walls absorbing signals, neighboring networks fighting for airtime, and dozens of client devices with varying capabilities all sharing the same access point.
Real-world throughput gets hammered by protocol overhead alone. Every data frame carries MAC headers, interframe spacing, and acknowledgments, and when you add TCP/IP encapsulation, retransmissions from collisions, and the half-duplex nature of most wireless links, you can easily lose 40 to 60 percent of the theoretical peak before any environmental factors come into play. Then there is the hidden node problem, where two clients cannot hear each other but both try to talk to the AP at the same time, forcing exponential backoff and further dragging down aggregate speed for everyone.
A helpful rule of thumb is to expect roughly half of the advertised rate under ideal real-world conditions, and often much less in dense or noisy environments. Instead of chasing the biggest number on the box, test with your own mix of clients, distances, and traffic patterns—especially if you rely on latency-sensitive applications like voice or video. The gap between a glossy spec sheet and what you actually get on a Tuesday afternoon with a dozen active users is often the difference between "it should work" and "it actually does."
FAQ
Buyers tend to fixate on line speed and ignore the corrugator block cooling design. Undersized cooling channels lead to warped walls on thicker pipe even at moderate outputs. Another hidden factor is vacuum tank length relative to your fastest speed—if it's too short, ovality becomes a daily fight.
Don't buy a machine where your most common size sits at the top of its range. Running near maximum diameter forces the molds to clamp at full pressure constantly, which causes uneven wall thickness. Pick a machine where your typical sizes fall in the middle third of its capability. That gives you better consistency and room to expand later.
Recycled HDPE with inconsistent melt flow index is the biggest headache—it causes surging and visible ring marks. High-melt-strength PP generally runs cleaner for deep profiles, but you need proper screw design. Always run trials with your actual production blend, not the clean virgin pellets suppliers use for demos.
Cleaning the corrugator block faces every shift is mandatory. Melt buildup changes profile shape quickly. Also drain the water separator on the vacuum pump twice a week—flooded separators destroy bearings. People often forget the hydraulic clamping filters until a mold sticks, so check those monthly.
A buffer zone between the corrugator and cutter is essential. Without it, every minor speed tweak creates tension that distorts the pipe. Look for integrated dancer control rather than manual synchronization. For perforated drainage pipe, place the punch unit after the pipe has cooled past the tacky stage to avoid tearing.
If you're unsure about demand, a single-wall machine with an optional inner liner die is cheaper to start. Double-wall lines cost 30–40% more but allow both solid and corrugated profiles via insert changes. Just remember that adding an inner layer later often requires a longer cooling section, so check your floor layout before committing.
Foundation leveling is critical. Even a 2 mm deviation over 20 meters pulls the pipe sideways and creates uneven walls. Also, don't share the compressed air line with other equipment—vacuum and mold clamping need stable pressure. Drops cause dropped molds and weak vacuum, which show up as random defects.
Yes, but the perforation unit needs its own frame and independent speed control. Cheap retrofits mount the punch station on the main haul-off, causing vibration that leaves ring marks. A properly integrated perforation head costs more upfront but avoids scrap and rework later.
Conclusion
A machine that runs beautifully with virgin HDPE may stumble the moment you feed it heavily recycled flake or a blend with inconsistent melt flow. The best corrugated pipe machine for your production needs starts with an honest look at your material mix. If your extruder and downstream corrugator cannot handle viscosity swings without surging or tearing, you will pay for it in downtime. Likewise, chasing headline output speed while your cooling and haul-off cannot maintain dimensional stability simply moves the bottleneck. High linear meters per minute mean little if wall thickness drifts and the pipe fails a crush test. Frequent die changes are another quiet profit killer: a corrugator that forces you to swap mold blocks for every diameter or profile change eats hours each week, and those hours rarely show up in a brochure.
Look instead for a corrugator with quick-change mold block systems and controls that adapt forming pressure and vacuum in real time. Smart controls do more than look modern; they cut scrap by catching thin spots and ovality before a full reel becomes waste. Long-life construction shows up in hardened wear surfaces, robust bearings, and a frame that does not flex under continuous high-cycle operation. Then compare real-world throughput: ask for reference runs with your own material, at your target wall thickness and pipe class, not a best-case demo with an easy grade. The right machine is the one that keeps producing spec pipe shift after shift, with less scrap and fewer changeovers, while your operators spend time running product instead of fighting adjustments.
Contact Us
Contact Person: LISA LEE
Email: [email protected]
Tel/WhatsApp: +86 13780696467
Website: https://www.qdpipemachine.com