China Bottom Pull Facial Tissue Machine Advantages for High Speed Production
2026-10-25
When high-speed output is non-negotiable, the design details of a bottom pull facial tissue machine matter more than ever. DAXIN builds China-sourced machines specifically engineered for rapid, continuous production—without sacrificing fold accuracy or paper handling. If you're evaluating your next upgrade, these advantages deserve a closer look.
Why Bottom Pull Design Handles Speed Better
The rear-facing cable entry isn't just a stylistic quirk—it shifts the balance point lower and closer to the pivot, cutting down on the wobble you feel when chasing a quick shift. With less cable flapping around the front, the derailleur reacts more directly to your thumb, especially when you're dumping gears mid-sprint.
Routing the housing along the down tube and under the bottom bracket keeps the cable run straighter and shorter than a top-pull setup. Fewer bends mean less friction and stretch, so the chain climbs the cassette without that vague, elastic lag that forces you to over-pull the lever.
On rough terrain, a bottom pull design also tucks the cable away from trail debris and errant heels. That protection translates into consistent tension over a long ride, letting you trust the shift instead of second-guessing the mechanism when the pace gets hot.
High Velocity Without Compromising Cut Quality
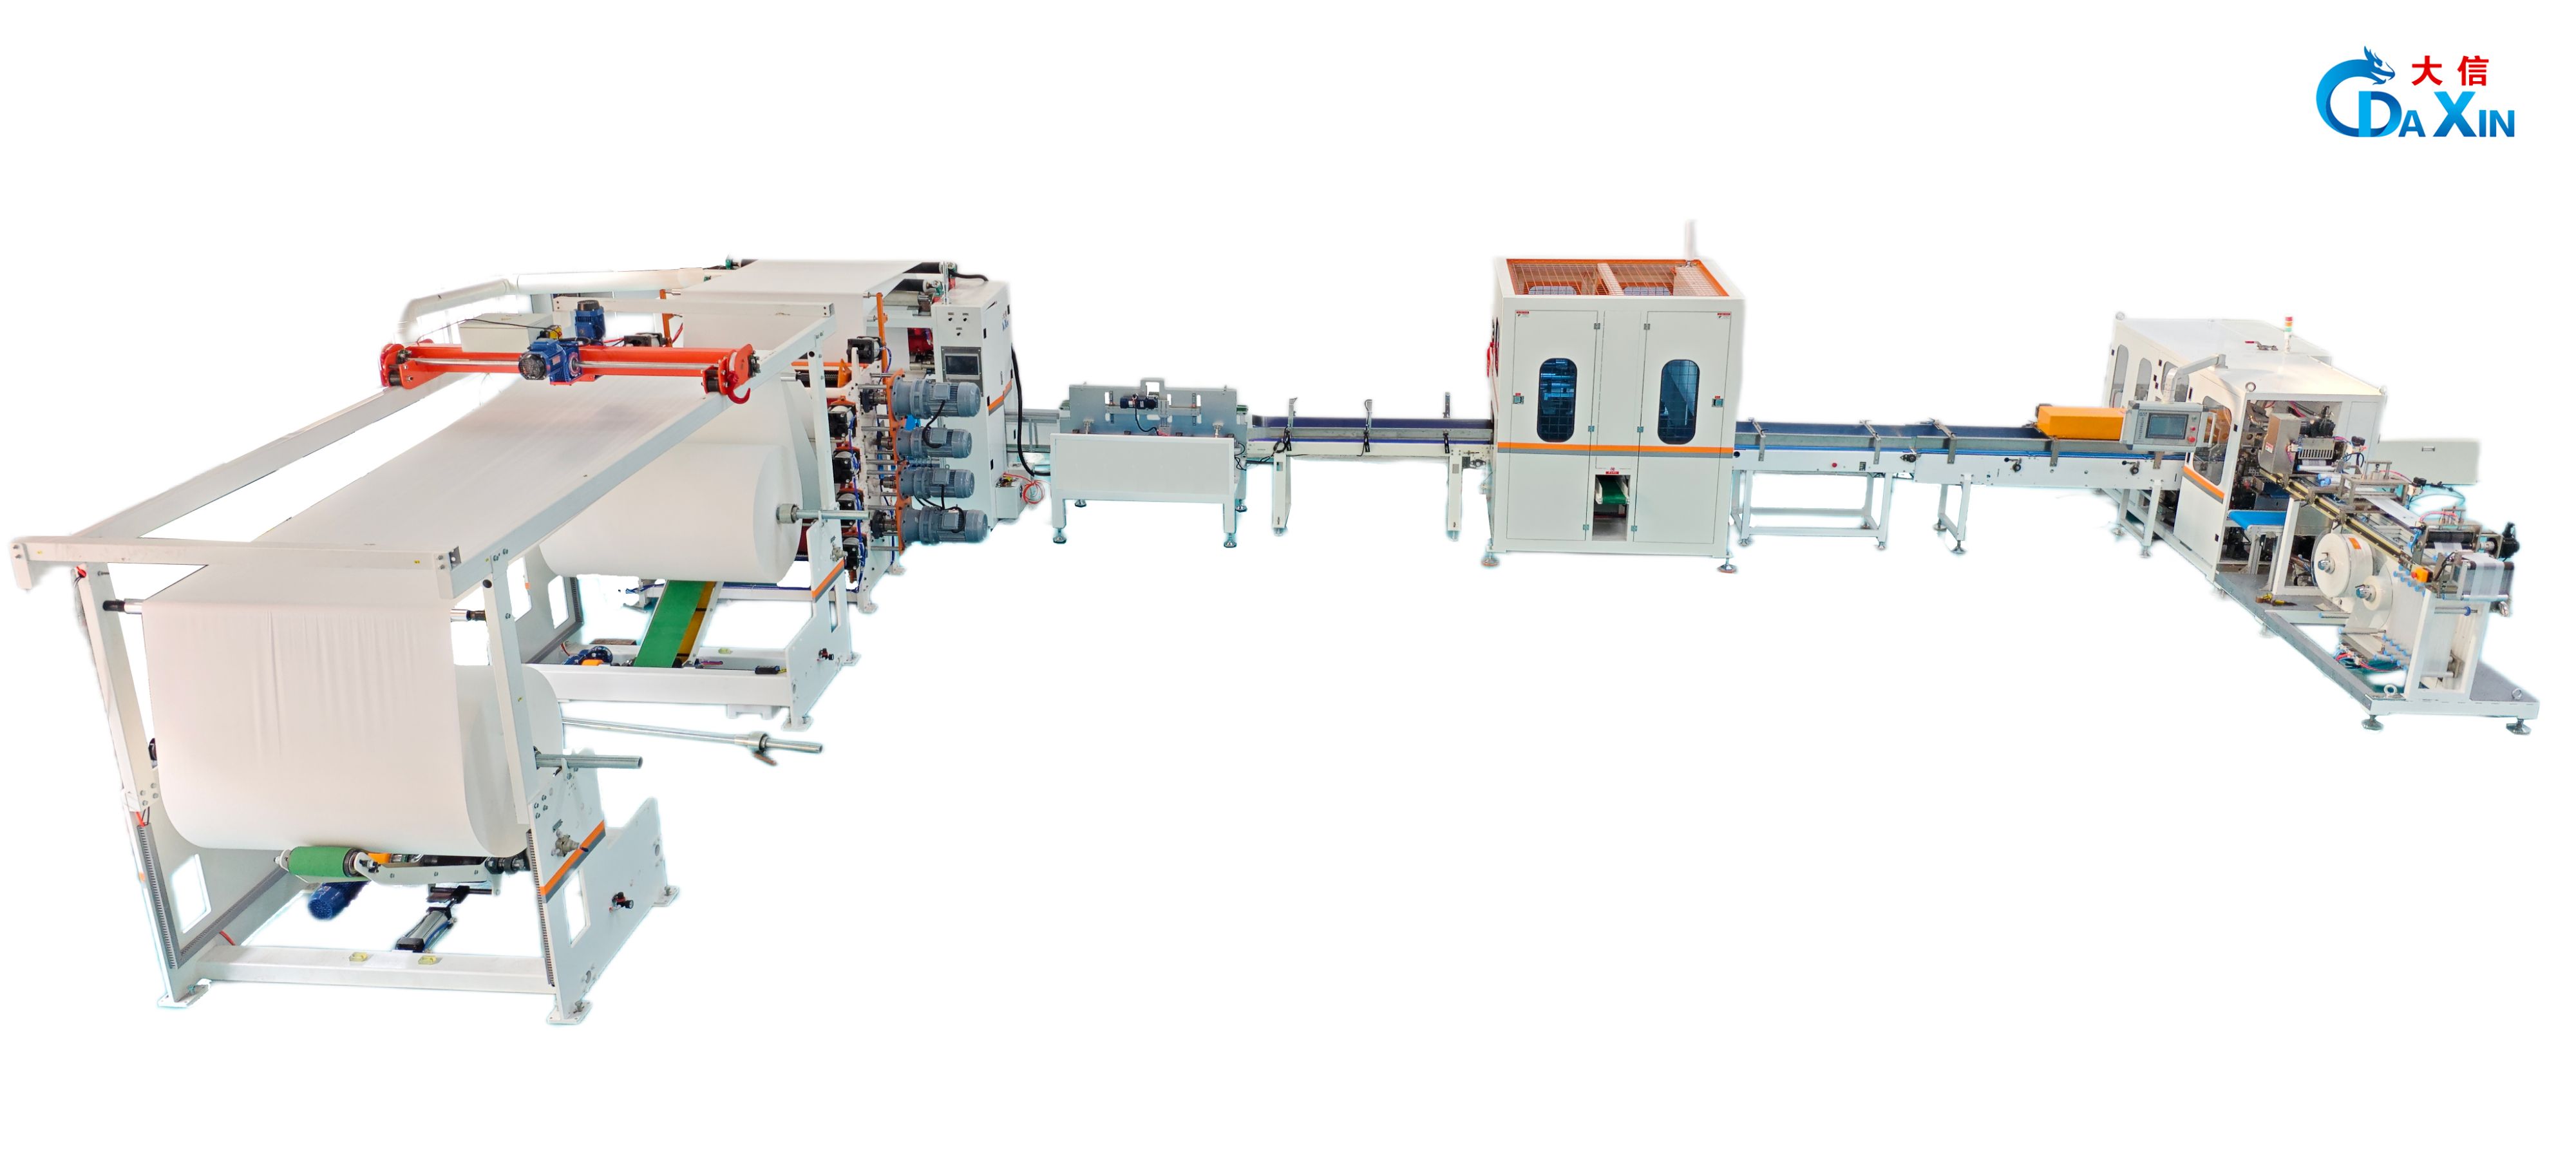
Speed in cutting usually comes with a penalty: rough edges, heat distortion, or wasted material. This system flips that expectation. The cutter head accelerates through straight runs and decelerates only where intricate geometry demands it, so linear paths are crossed at full throttle without ever letting the kerf wander. The result is a rate of production that feels almost aggressive, yet every finished piece drops off with a clean, square edge.
What makes the velocity sustainable is the adaptive motion control. Instead of a fixed speed limit for the entire job, the drive reads upcoming contours in real time and adjusts feed rate on the fly. Tight corners get the precision they need, while long stretches receive every bit of available speed. It is not a compromise between fast and accurate; it is a merger of both, tuned per geometry rather than per material batch.
Operators often notice the absence of chatter or secondary sanding. That is the real payoff. High travel speed does not force you into rework, because the cut quality remains identical to slower, more conservative passes. You gain throughput without adding a finishing step, which changes how you schedule entire production runs.
Built for Continuous Duty, Not Just Peak Numbers
Most machines look impressive on a spec sheet, but real work doesn't happen in short sprints. This unit is engineered to hold its rated output hour after hour without thermal throttling or premature wear. The cooling path, bearing selection, and winding insulation are all sized for sustained stress, so you get the same dependable performance at 3 a.m. as you do in the first five minutes.
We test differently because we know downtime costs more than any headline number. Prototypes run extended duty cycles at full load in ambient temperatures that mimic cramped equipment rooms and sun-baked enclosures. If a component starts to drift, it gets redesigned before it ever reaches your floor. That's the difference between a unit that posts a strong peak and one that carries the load all year.
The result is a quieter, cooler, and more predictable workhorse. You won't need to de-rate it for summer heat or schedule extra maintenance just to keep it alive. It simply runs, shift after shift, without drama.
Fewer Stoppages Translate to More Finished Packs
On a busy packaging line, even a two-minute stoppage is rarely just two minutes. It breaks the rhythm that operators and conveyors settle into, forces someone to walk over and inspect a jammed carton or a misaligned film, and often leaves a few half-finished packs that have to be scrapped. When these micro-interruptions happen several times per shift, the lost output isn't trivial—it can easily add up to hundreds of packs that never make it to the pallet.
Reducing stoppages doesn't always call for major equipment upgrades. Many frequent pauses come from small things: a sensor that trips too easily, a belt that slips at a certain speed, or a feed roller that runs empty for a second longer than it should. Fixing these issues keeps the line in a longer, steadier run. And the longer the line runs without interruption, the closer each shift gets to its real capacity, which is how fewer stoppages directly become more finished packs.
China-Based Engineering Cuts Downtime and Lead Times
Local engineering teams in China work directly with production lines, often on the same campus or within a short drive. This proximity eliminates the delays that come with coordinating across time zones or waiting for overseas support. When a mold needs adjustment or a fixture fails, engineers can be on the floor within hours, not days. The result is a measurable drop in unplanned downtime, because potential bottlenecks are spotted and addressed before they escalate into full stops.
Shorter lead times come from more than just speed; they come from iteration without friction. A design tweak requested in the morning can be prototyped, tested, and approved by the afternoon, then fed directly into the next production run. There is no long email chain, no customs clearance for sample parts, no re-explaining requirements to a distant team. This tight loop compresses the timeline from concept to finished component, giving customers a real advantage when their own schedules shift or demand spikes.
What often gets overlooked is the practical knowledge embedded in these local teams. They understand the quirks of regional material suppliers, the limits of specific CNC machines, and the nuances of surface finishing that only come from daily exposure. That depth of familiarity reduces rework, which in turn keeps both downtime and lead times low. Instead of relying on generic workflows, the engineering process adapts to the actual conditions on the ground, making the entire operation more resilient and responsive.
Operator-Friendly Controls Keep Output Consistent
The control panel doesn’t bury the settings that matter. A clearly labeled dial for speed, a separate toggle for feed rate, and a dedicated start/stop button mean operators spend less time hunting through menus and more time watching the actual output. When adjustments are needed mid-run, the changes take effect immediately without requiring a full stop, so minor drift gets corrected before it becomes scrap.
What really keeps output consistent is the ability to lock in proven recipes. Once a setup produces the desired finish, a supervisor can save those exact parameters under a simple name. Floor workers then load the recipe with two taps—no guesswork, no accidental offset. Password protection on critical thresholds stops unauthorized tweaks that often lead to batch-to-batch variation.
FAQ
The main difference lies in the servo-driven folding and cutting units that sync precisely with the bottom pull format. Unlike older cam-driven designs, these machines keep web tension steady even above 160 packs per minute, so jams stay rare and the tissue edges remain crisp.
Bottom pull means the tissue is drawn from the lower layer of the stack, which reduces the chance of double-pulling at high speeds. The pickoff uses a vacuum belt with timed release, so each tissue separates cleanly without slowing the line down for misfeeds.
Entry models usually run at 100 to 120 packs per minute, while heavy-duty versions with reinforced frames and rotary valves can sustain 180 to 200 packs per minute. The actual speed depends on ply count and fold type, but the upper range is where the bottom pull design shows its advantage.
The critical areas are the folding plates, rotary cutting knives, and vacuum pickoff rollers. Chinese manufacturers often use tungsten carbide-coated blades and oversized bearings on the main shafts. That combination reduces heat buildup and lets operators run three shifts without frequent bearing swaps.
Yes, most modern bottom pull machines have servo-driven folding bars and quick-change cassettes. You can move from 2-ply to 3-ply or switch from C-fold to V-fold in under twenty minutes. Because the settings are recipe-based, the machine returns to its target speed without trial-and-error adjustments.
Daily checks focus on the vacuum pump filters, folding plate alignment, and pickoff belt tension. If those three stay within tolerance, the machine holds its speed and fold accuracy. Weekly lubrication of the cam followers and monthly inspection of the timing belts prevent most surprise shutdowns.
The upfront cost is typically 40 to 50 percent lower, but the real reason is lead time and spare parts support. Chinese suppliers can ship a configured machine in six to eight weeks and keep common wear parts in local warehouses. Since the bottom pull design has fewer complex indexing parts, it also costs less to repair after the warranty period.
Conclusion
The bottom pull configuration changes how the sheet leaves the folding unit. Instead of pulling upward against gravity and drag, the web is drawn downward along a shorter, more direct path. That reduces tension spikes at high line speeds, so the machine can accelerate past 1,000 cuts per minute without tearing thin sheets or losing fold registration. The cut quality holds up because the rotary knife and servo-driven feed are timed by the same motion controller, not by a mechanical clutch. You get clean edges on both virgin and recycled stock, which matters when buyers check pack appearance at retail.
Continuous duty is where most machines fall short. Here the frame is heavier, the gearbox is oil-cooled, and the vacuum ports are oversized to avoid clogging on lint. Fewer stops mean more finished packs per shift; operators rarely need to clear jams or rethread. Since these lines are engineered and assembled in China, spare parts and technical support arrive faster, and custom modifications—like changing fold width or pack count—don't require months of back-and-forth. The control panel uses a touchscreen with recipe memory, so a shift change doesn't change the setup. One operator can monitor several lines and still keep output within tight tolerances.
Contact Us
Contact Person: Sam Xie
Email: [email protected]
Tel/WhatsApp: 86-18938538530
Website: https://www.daxin321.com/