Custom PTFE Envelope Gaskets for Durable Sealing Performance
2026-10-29
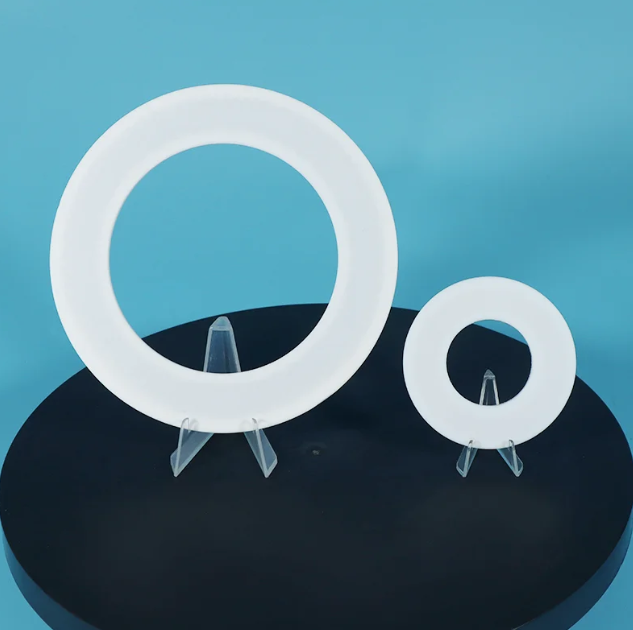
Leaks can cripple even the most carefully designed system, especially when aggressive chemicals or extreme temperatures come into play. That’s where the right gasket makes all the difference—and not just any gasket. Custom PTFE envelope gaskets combine a resilient core with a chemically inert PTFE shell, delivering durable sealing performance where conventional materials fail. Whether you're dealing with corrosive media or demanding flange conditions, TAIFNO specializes in tailoring these gaskets to your exact specifications. In this post, we'll break down why PTFE envelope gaskets stand out and how custom configurations can solve sealing challenges that off-the-shelf options simply can't.
What a Custom PTFE Envelope Gasket Does Differently Under Heat Cycling
Most standard envelope gaskets struggle under repeated heating and cooling because the PTFE skin and the core expand and contract at different rates. A custom design addresses this by selecting a core material whose thermal expansion sits closer to the PTFE’s range, and by adjusting the envelope overlap or thickness so the softer PTFE layer is not pulled apart at the corners.
During thermal cycling, PTFE has a tendency to creep or flow away from high-load zones, especially around the inner edge. A custom envelope gasket can incorporate a more creep-resistant PTFE grade or a slightly thicker wall on the ID side, which keeps the seal tight after dozens of cycles instead of gradually losing bolt load.
The real difference shows up in recovery. Off-the-shelf gaskets often take a compression set after the first hot soak and never fully spring back when the flange cools. A custom profile can be machined or molded with a controlled envelope taper and a resilient core, allowing the gasket to follow flange movement and maintain contact stress even when the faces bow or shift.
Choosing a Core That Won't Bottom Out Before the Envelope Seats
In speaker driver design, the voice coil former (often called the core) can hit the back plate before the winding edges—the envelope seats—reach their travel limit. That premature contact destroys the coil and sounds terrible. So the first step is to stop guessing and measure the actual excursion at the driver's rated power. Many builders assume the published Xmax tells the whole story, but real-world peaks often exceed it by 20 percent or more. Use a laser displacement sensor or a simple marked dowel to capture the worst-case movement, then add a safety margin of at least 15 percent.
Once you know the true peak excursion, you can work backward from the envelope seats. Mark the exact position where the winding ends on the former, then compute the gap needed between that point and the back plate at full excursion. A common mistake is to make the former too short, hoping to save weight; that shifts the bottoming point to the bare former, which has no cushioning. Instead, extend the former past the winding end by a distance equal to your measured excursion plus the safety margin. Also consider using a former material like anodized aluminum or high-temp polyimide that resists buckling when it does make light contact.
Finally, test under realistic conditions—not just a sine sweep. Play bass-heavy music or a burst signal at the driver's thermal limit for at least 30 minutes. Watch for any tick or mechanical noise that indicates the former is hitting before the envelope seats. If you hear it, increase the former length or reduce the rearward travel with a slightly stiffer spider. The goal is not to eliminate all contact, but to ensure that when contact does happen, the winding edges absorb the impact instead of the core. That way the driver survives long-term abuse without losing its voice.
Machining the Envelope Lip: Small Radius, Big Leak-Prevention Payoff
The envelope lip gets its name from the way it wraps around the mating surface, and that small radius at the edge does more work than it gets credit for. A 0.15 mm radius, for instance, changes how the seal contacts the shaft—spreading pressure more evenly instead of letting it spike at a sharp corner. That tiny geometry is often the difference between a dry housing and a slow weep.
Machining that radius reliably is the hard part. Tool deflection, chatter, and heat buildup all show up at this scale, and a few microns of error can leave a lip that looks fine on paper but leaks under load. Shops that hold this feature tight usually switch to CBN inserts or finish with a rigid boring bar, checking the profile under magnification rather than trusting a standard radius gauge.
When the envelope lip is machined correctly, the payoff shows up in the field. Seal life stretches out because the contact band stays consistent, and warranty claims for seepage drop noticeably. It is not a glamorous feature to machine, but it is one of those small details that quietly keeps hydraulic and rotating equipment running longer.
Installation Torque Sequences That Keep the PTFE Envelope Intact
Getting the torque sequence right is the single most overlooked step when installing PTFE envelope gaskets. A standard crisscross pattern works, but only if you treat every pass as a halfway point, not a finish line. Start by snugging the bolts finger-tight, then bring each one to roughly 30% of the target torque in a star or diagonal pattern. Stop there and check the gasket visually: the envelope should still look relaxed, with no folds or shiny stretch marks. If you see even a hint of the envelope pulling away from the core, back off and reset that bolt before moving forward.
From 30%, climb in 20% increments and always follow the same pattern direction, never jumping across the flange. This keeps the load even and lets the PTFE flow slowly into surface imperfections without tearing. The final pass should land every bolt within a 5% window of the rated torque, not just the one you touched last. Resist the urge to do a final “snug check” after a minute or two—re-torquing a settled PTFE envelope often breaks the cold-flow bond that has just formed and is one of the fastest ways to split the material at the bolt circle.
Spotting Cold Flow Early: Field Checks That Save Flange Faces
Cold flow rarely announces itself with a dramatic leak. More often, the gasket material has already started creeping out from between the flanges long before the first drip appears. On a routine walkdown, run your fingers along the outer edge of the flange joint where the gasket should be flush. If you feel a slight ridge or a bead of material that wasn't there during the last inspection, that's the gasket extruding under load. Pay extra attention to non-metallic and PTFE-based gaskets, since they cold-flow at much lower stress levels than spiral-wound or ring-joint types.
A second check is to look at the gap between flange faces. Use a feeler gauge at three or four points around the circumference. The readings won't be identical on every joint, but a difference of more than a few thousandths of an inch from one side to the other often means the gasket has thinned unevenly. This is especially true on flanges that have been retorqued multiple times without replacing the gasket. The bolts may still feel tight, but the residual load on the gasket can be nearly zero in the middle of the span.
Don't ignore fastener clues either. A stud that has stretched slightly or a nut that turns a hair before breaking friction can signal that the joint has lost compression. Mark the nut-to-flange position with a paint pen during the next shutdown. If the marks have shifted on a live system, you have movement. Catching these signs early means you can schedule a re-torque or gasket replacement before the flange face itself gets chewed up. Once the face is grooved or pitted from a hardened gasket, the repair cost jumps well beyond a simple gasket swap.
When a Custom Envelope Outperforms Filled PTFE and Rubber Composites
Filled PTFE and rubber composites hold up under predictable loads, moderate temperatures, and clean media. But the moment a flange starts to flex, a housing develops uneven bolting stress, or the chemical stream swings between aggressive solvents and hot acids, those uniform materials start showing their limits. A custom envelope—typically a PTFE or modified-PTFE shell wrapped around a compressible core—absorbs that movement without sacrificing the wetted surface. The core keeps the seal live under low bolt load, while the envelope resists attack from media that would swell, crack, or leach plasticizer out of a rubber sheet.
That combination becomes decisive in glass-lined equipment, thin-walled piping, and reactors where torque is limited. Rubber composites often need high compressive force to seal, and filled PTFE can creep or cold-flow until the gasket loses thickness. A well-designed envelope spreads the available load more evenly, rebounds after thermal cycling, and can be tailored with different core materials to match precise compressibility targets. When a standard sheet starts leaking after a few temperature swings or a process change, the custom envelope is often the retrofit that stops the drip without requiring a flange redesign.
FAQ
They consist of a machined or molded PTFE shell wrapped around a compressible core, combining chemical resistance with the resilience needed to maintain a tight seal under fluctuating temperatures and pressures.
Yes, customization covers diameter, thickness, bolt hole patterns, and even unusual shapes like oval or rectangular, so they match your exact flange face without forcing a standard size.
Chemical processing, pharmaceutical manufacturing, food and beverage, and pulp and paper plants often use them where aggressive media would degrade conventional rubber or fiber gaskets.
Common choices include solid PTFE, filled PTFE, elastomeric inserts like EPDM or Viton, and corrugated metal cores, each balancing compressibility, creep resistance, and temperature range differently.
The PTFE outer layer withstands temperatures from roughly -200°C to +260°C, while the core supports sealing pressure, but actual limits depend on the specific core and flange design.
The envelope construction protects the core from chemical attack and prevents cold flow of pure PTFE, so the gasket retains its thickness and sealing force over more thermal cycles.
Use controlled torque and follow a star pattern to avoid uneven compression, and avoid overtightening because the PTFE shell can deform if the core bottoms out.
Yes, many suppliers can reverse-engineer from a sample or CAD drawing, producing a drop-in replacement with the same dimensions and core configuration.
Conclusion
Under repeated thermal swings, a custom PTFE envelope gasket behaves differently than a solid sheet or filled grade. The envelope flexes with the flange movement instead of taking a set, so the sealing contact stays alive after dozens of cycles that would crush a standard gasket. But that only works if the core is selected for compressive stiffness below the envelope's seating stress—many failures come from a core that bottoms out first, leaving the PTFE lip unloaded. A small machined radius on the envelope lip matters more than it looks: it prevents a sharp crease from splitting at the inner edge, which is where most weepage starts. Getting that radius right lets the lip conform to minor flange irregularities without cutting itself.
Installation torque has to be staged and even, not just hit a final number. Uneven bolt-up can tear the thin PTFE envelope along the outer edge before the gasket ever sees process pressure. Once in service, catching cold flow early saves the flange faces—look for PTFE squeezing past the flange OD or a drop in bolt load at regular intervals. If you spot extrusion before it hardens, you can re-torque or swap the gasket instead of dealing with eroded flange serrations. Compared to filled PTFE or rubber composites, a custom envelope typically holds up better when the chemical exposure is too aggressive for rubber and the temperature range is too wide for filled PTFE to stay elastic. The right combination of core, lip geometry, and joint procedure gives a longer mean time between resealing without exotic materials.
Contact Us
Contact Person: Tommy Xiao
Email: [email protected]
Tel/WhatsApp: 8615651509888
Website: https://www.ptfe-factory.com