Expansion Shell Bolt Manufacturer Tips for Reliable Concrete Anchoring
2026-11-02
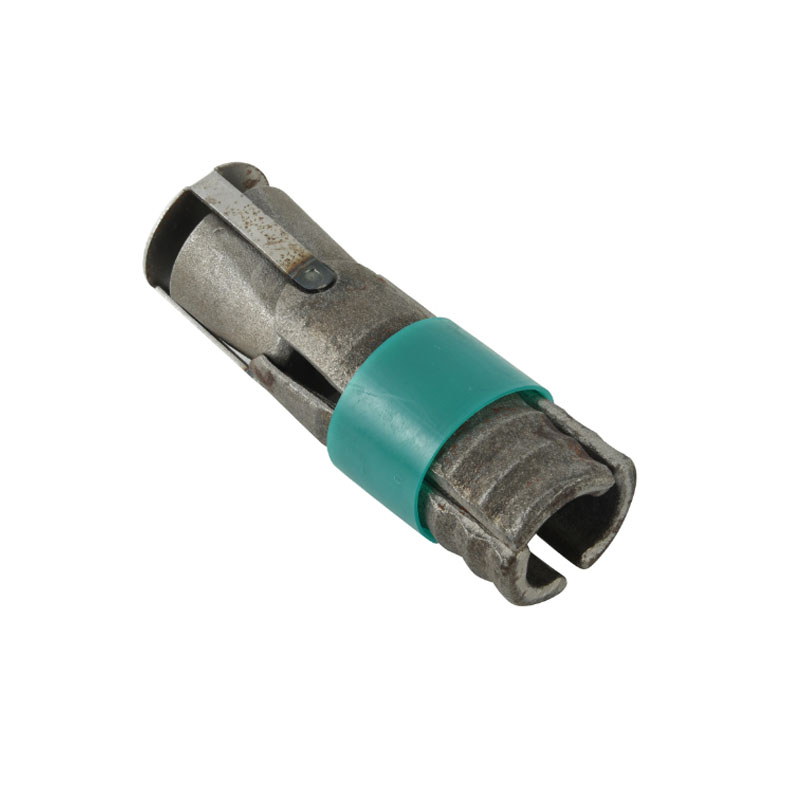
Concrete anchoring failures are often traced back to one overlooked detail: the expansion shell bolt. Whether you're securing heavy machinery or structural supports, a reliable hold starts with understanding how these bolts interact with concrete under load. As a trusted Supreme Machinery manufacturer, we've seen firsthand where installers go wrong and how small adjustments make a big difference. In this guide, we break down practical tips that improve pull-out strength, reduce cracking risks, and extend service life—without adding complexity to your workflow.
Raw Material Choices That Make or Break Holding Power
The backbone polymer isn't just a carrier; its molecular weight distribution and crosslink density quietly dictate whether an adhesive creeps under load or holds firm. A resin with too many low-molecular-weight chains might wet a surface beautifully at first, but those short chains can slip past each other over time, leading to gradual shear failure. Manufacturers often chase tack with softer grades, yet that softness has to be anchored by enough high-molecular-weight fraction to resist cold flow.
Tackifiers are where many formulations go wrong. They boost initial grab, but if the tackifier isn't fully compatible with the base polymer, it will migrate to the interface or form a separate phase after aging. That phase separation doesn't just reduce clarity—it creates weak boundary layers that peel away under sustained load. The best holding power usually comes from using a tackifier with a similar solubility parameter to the polymer and keeping the loading below the point where the glass transition rises too sharply.
Fillers and rheology modifiers can either reinforce the adhesive network or simply dilute it. Fumed silica, for instance, builds a three-dimensional network that resists flow, but over-dosing turns the adhesive brittle and reduces its ability to wet rough substrates. Carbon black adds UV stability but can absorb plasticizer and shift the viscoelastic balance. The key is to test holding power at the actual service temperature, because a formulation that feels strong at room temperature might soften dramatically on a hot roof or inside a sun-exposed panel.
Reading the Concrete Before You Drill: What Most Guides Skip
You can own the fanciest hammer drill on the market, but if you misread the slab, you'll still end up with a wandering bit, a cracked edge, or a hole that's just slightly off from where it needs to be. Most guides jump straight to tool settings and anchor types, skipping the part where you actually look at what's in front of you. Concrete isn't a uniform gray mass. Age, aggregate distribution, surface hardness, and even the presence of hairline cracks all change how the bit bites. Run your hand over the surface first. Feel for patches that are denser or more porous, for old patch repairs that might hide voids, or for areas where the finish has spalled away. That tactile check tells you more than any spec sheet ever will.
Another detail that gets ignored is the sound test. Tap the concrete lightly with a hammer or the butt of a screwdriver. A sharp, ringing note usually means a solid, dense area that will drill cleanly but may wear your bit faster. A dull, hollow thud suggests a void, a delaminated section, or a spot where aggregate has settled poorly. Drilling into that hollow zone can cause the bit to grab suddenly, chip out a larger crater than intended, or even punch through into an unexpected gap behind the slab. If you hear that dull sound, shift your mark an inch or two—if possible—or prepare for slower feed pressure and a backing board to prevent blowout.
Finally, look at the surface texture under raking light. Minor undulations, old trowel marks, or a light dusting of laitance can all deflect a starting bit. Professionals sometimes scratch a tiny cross at the drill point with a nail or a center punch, giving the bit a groove to seat into before the hammer action kicks in. Without that, a bit on a smooth, hard floor can skate sideways, leaving a crescent-shaped scar that's almost impossible to hide. It's a ten-second step that most how-to articles never mention, but it's the difference between a hole that looks intentional and one that looks like a repair job waiting to happen.
Hole Geometry: Why a Few Millimeters Change Everything
A drill bit doesn't just remove material. It negotiates with everything around it. Push the diameter out by two millimeters and you've altered the stress distribution across the entire component, not merely widened a passage. In precision assemblies, that tiny increment can shift a press-fit into a slip-fit, invite vibration where there was none, or quietly steal away the fatigue life of a bracket that looked perfectly adequate on paper.
The real trap is thinking of a hole as a simple negative space. Every edge introduces a notch effect, every countersink changes how a fastener seats, and every slight mismatch between drill wander and reamer tolerance creates a stress riser that no finite element model will warn you about unless you've already learned to look for it. Those few millimeters dictate whether a seal holds, whether a dowel aligns under load, or whether an oil gallery starves a bearing at exactly the wrong RPM.
Seasoned machinists know the feel of it: the moment a hole stops being a hole and becomes a functional cavity with its own taper, roundness error, and surface finish signature. Change the depth-to-diameter ratio, the entry angle, or the breakthrough burr behavior, and you've changed how the part behaves in service. That's why drawings that treat a hole merely as a dimension are missing the story—the geometry is the entire plot.
Torque Is Not a Suggestion: Getting Tightening Right
Every fastener has a specified torque for a reason. It's not a starting point for negotiation or a loose guideline you can ignore when the wrench feels tight enough. Exceeding it by even a small margin can stretch bolts past their yield point, while under-tightening invites vibration loosening and joint failure.
The problem with "feel" is that human perception of tightness varies wildly with tool length, grip position, and fatigue. A calibrated torque wrench removes that guesswork, but only if you use it correctly. Pull smoothly until the click, stop immediately, and never use extensions that alter the lever arm unless you've recalculated the setting.
Thread condition matters more than most people realize. Dry, lubricated, or anti-seized threads all require different torque values to achieve the same clamp load. Ignore that, and you're back to guessing with an expensive tool in your hand.
Spacing and Edge Distances You Can’t Afford to Ignore
In structural connections, the distance from the center of a fastener to the edge of the material—and the spacing between fasteners—directly controls how load travels through the joint. A bolt placed too close to a concrete edge doesn’t just look awkward; it can trigger a cone-shaped breakout failure at a fraction of the design load. That’s because the surrounding material needs enough mass to resist the tensile and shear forces trying to pull or push the anchor out. Once edge distance falls below the required minimum, the failure mode shifts from ductile steel yielding to brittle concrete fracture, which gives little warning before collapse.
Site crews often underestimate how quickly small adjustments add up. Moving a row of anchors an inch inward to dodge rebar might seem harmless, but it can put every fastener below the specified edge distance. The result is a connection that passes visual inspection yet carries only 60 or 70 percent of its intended capacity. Similarly, crowding fasteners too closely causes overlapping stress cones, so the group behaves like one oversized hole rather than a distributed connection. These are not theoretical risks—they show up as chipped edges during tightening, hairline cracks after service loads, or anchors that slowly loosen over time.
On site, the rule comes down to this: verify the minimum edge and spacing dimensions before drilling, not after. When a conflict with reinforcement or formwork forces a change, flag it for the engineer instead of shifting the layout on the fly. A few extra minutes of layout work preserves the designed failure mechanism and keeps the connection’s strength predictable. In renovation work, where existing concrete edges may be irregular or damaged, assume nothing—measure each anchor location independently and adjust the pattern to maintain full edge distance, even if it means adding a steel plate or changing the anchor type.
Proof Testing Anchors: Cheap Insurance Against Failure
A proof test on a wedge anchor isn't a lab exercise. It's a hydraulic ram, a calibrated gauge, and a few minutes of watching whether the anchor creeps under load. That small ritual catches the failures that torque alone misses: a hole drilled slightly oversized, dust left in the bore, a batch of concrete that cured softer than the drawings assumed. None of these show up when you tighten the nut. They show up when you pull to 125% of working load and the anchor starts to walk out of the hole.
The cost side is almost embarrassing. A basic test kit and a competent operator can proof a dozen anchors before lunch, and the whole procedure costs less than replacing a single stripped insert after the steel is up. Compare that to the alternative: a failed anchor discovered when a hoist line goes taut or a handrail gets bumped. At that point you're not paying for a test; you're paying for cleanup, down time, and someone's explanation of why the cheap step was skipped.
FAQ
Drill the hole at least the bolt embedment depth plus a little extra for dust, usually 1/4 to 1/2 inch deeper than the anchor length. Clean out debris with a blow pump or brush before inserting the bolt, because leftover dust can prevent the shell from expanding fully and reduce holding power.
Keep a minimum edge distance of about 5 to 10 times the bolt diameter from the concrete edge, and use a torque wrench to avoid overtightening. Overtorquing creates radial stress that can split the concrete, especially in lower-strength slabs or near corners. If you must anchor close to an edge, consider reduced-torque settings or a different anchor type.
Generally no. Expansion shell bolts rely on wedging against solid material, so hollow cores or lightweight block webs don't provide enough continuous bearing area. For those substrates, use a through-bolt with a plate or a chemical anchor designed for hollow base materials.
The exact torque depends on bolt diameter and concrete strength, but as a rule, tighten until the shell seats firmly and then apply the manufacturer's recommended torque from a calibrated wrench. On typical 1/2-inch bolts in 3,000 psi concrete, this is often around 40 to 50 ft-lbs, but always check the spec sheet because overtorque is a common cause of anchor failure.
Check the hole cleanliness, drill bit wear, and concrete strength. A worn bit can produce an undersized hole, and dust left in the hole can cushion the expansion. Also verify that the embedment depth meets the load requirements and that you're not using the bolt in cracked concrete unless it's rated for that condition.
A rotary hammer is preferred because it produces a cleaner, more consistent hole with less walking and less bit wobble. A hammer drill can work for small diameters, but in hard aggregate or deep holes it may create an irregular bore that reduces contact between the shell and concrete, lowering the anchor's capacity.
Test the concrete's compressive strength, typically by reviewing the project's cylinder test reports or using a rebound hammer for an approximate check. Expansion shell bolts perform best in concrete rated 3,000 psi or higher. If the surface crumbles easily under a scratch test or if the concrete is old and deteriorated, choose a different anchoring method.
Conclusion
Ask any expansion shell bolt manufacturer where jobs go wrong and they’ll point to the same handful of shortcuts. Raw material choices make or break holding power: cheap steel shells with poorly hardened expansion leaves deform before they bite, while matched alloy wedges and cones allow consistent expansion. Reading the concrete before drilling is just as critical—green concrete, lightweight block, and aged cracked slabs all behave differently, and the feel of a hammer drill can reveal whether you're hitting solid aggregate or a hidden void. Hole geometry then becomes the silent killer; a few millimeters oversize or a dust-filled hole lets the shell spin instead of expanding. Brush, blow, and measure every single hole.
On the tightening side, torque is not a suggestion. Under-tightening leaves the wedge only partially engaged, and over-tightening can strip the cone or fracture the concrete. Use a calibrated wrench and follow the manufacturer's range exactly. Spacing and edge distances also refuse to be ignored—anchors placed too close together or near a free edge develop overlapping stress cones that lead to cracking. When in doubt, follow the datasheet, not your instincts. Finally, proof testing a handful of anchors per job is cheap insurance: load them slightly above design load and watch for movement. If an anchor creeps, stop, pull it, and reassess rather than praying it holds. That discipline is what separates reliable anchoring from expensive callbacks.
Contact Us
Contact Person: Paul
Email: [email protected]
Tel/WhatsApp: 8615067447509
Website: https://www.spironcasting.com