Far Infrared Heating Reactor Manufacturer Delivers Precision Thermal Solutions
2026-09-21
For chemical processes where even a few degrees of deviation can ruin an entire batch, conventional heating methods often fall short. That’s where the far infrared heating reactor technology from Shenzhou Chemical Industry changes the game—delivering precision thermal solutions that keep reactions stable, efficient, and repeatable. In this post, we’ll explore how this advanced heating approach can elevate your production line.
Precision Thermal Control in Far Infrared Reactor Design
In far infrared reactor design, uneven thermal distribution remains a primary obstacle to consistent yield and selectivity. Conventional heating elements often create hotspots near the emitter while leaving peripheral zones underheated. Precision thermal control shifts the design away from a single heat source toward independently regulated zones, each with its own power modulation tied to real-time temperature feedback. This approach flattens the thermal gradient across the reaction cavity without relying on oversimplified uniform heating assumptions.
The core of precision control lies in sensor placement and control logic. Embedding miniature thermocouples or fiber optic sensors into the reactor wall and internal support structures produces a dense thermal map rather than a few scattered readings. A model predictive controller, unlike a standard PID loop, accounts for the thermal inertia of the ceramic emitter and the wavelength-dependent absorption depth of far infrared radiation. By anticipating thermal lag, the controller adjusts output before the temperature deviates, keeping transient fluctuations within a narrow band during ramp-up and cool-down phases.
Material choices further sharpen control accuracy. Using a low-expansion ceramic substrate as the infrared emission carrier reduces dimensional drift that would otherwise alter radiative geometry. Coating the reflector with a high-reflectivity metallic film minimizes stray radiation and thermal crosstalk between adjacent zones. When combined with adaptive zone weighting, these hardware refinements enable temperature stability within ±0.5°C across a broad load range, a critical requirement for heat-sensitive synthesis where even minor drift can change reaction pathways.
Custom Heating Jackets That Fit Existing Process Lines
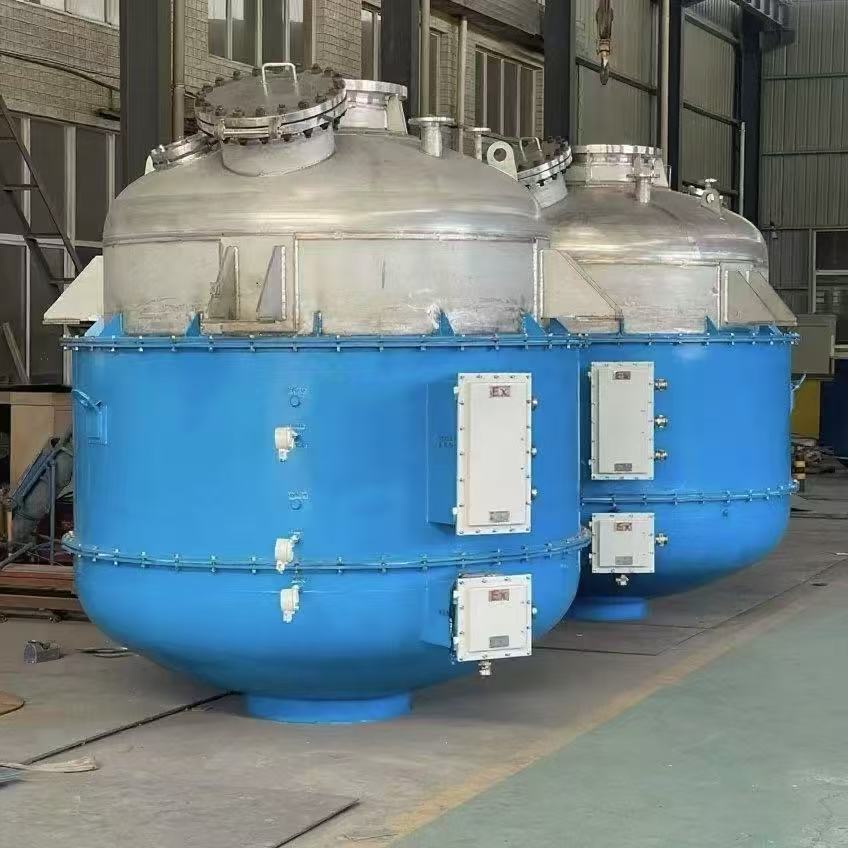
Retrofitting heating jackets onto process lines that were never designed for them used to mean compromising on fit, performance, or both. Standard off-the-shelf options leave gaps around valves, flanges, and odd-shaped vessels, forcing maintenance crews to improvise with loose wraps or excessive insulation. Custom heating jackets flip that approach: every bend, port, and bracket is measured directly from your existing line, so the jacket hugs the surface without air pockets or hot spots. The result is a heater that behaves like part of the original system, not an afterthought strapped on in the field.
The real advantage shows up during installation and long-term operation. Because each jacket is cut to match the exact profile of your equipment, you skip the time usually lost to trimming, shifting, or re-securing generic pads. Sensors, drains, and access points are left uncovered exactly where needed, while the heated surface remains continuous elsewhere. Operators notice fewer cold zones and less energy waste, since the custom pattern eliminates the small gaps where heat normally leaks away. Over months of cycling, the consistent contact also reduces thermal stress on flanges and welds compared to loosely fitted alternatives.
No two process lines are identical, so the design phase starts with photos, drawings, or a simple field sketch—not a catalog number. That flexibility lets you handle unusual pipe diameters, asymmetric pump housings, or crowded manifolds without forcing a square peg into a round hole. The jacket's outer shell, insulation thickness, and heating element layout can be adjusted to match the line's temperature requirements and chemical exposure. For plants running multiple older assets, this means one supplier can deliver consistent heating across the entire system while still fitting each piece precisely as it stands today.
Reducing Thermal Gradients Across Catalytic Beds
Thermal gradients across catalytic beds can quietly undermine reactor performance. When one region runs hotter than another, reaction rates drift out of sync, selectivity drops, and in severe cases the catalyst itself degrades unevenly. A common culprit is uneven flow distribution or non-uniform heat removal, which turns a well-designed bed into a patchwork of micro-environments.
Practical mitigation starts with rethinking inlet and outlet configurations. Angled baffles, perforated distributors, or radial-flow geometries help spread the feed more evenly, while staged cooling or inter-bed heat exchangers can pull heat away before it accumulates. Even simple changes—like adding a thin layer of inert packing at the hot spots or adjusting particle size near the wall—can flatten the temperature profile without a full redesign.
Monitoring matters too. Temperature probes placed at multiple axial and radial positions give an early warning of gradient buildup. Instead of waiting for a hotspot to trip an alarm, operators can compare real-time profiles against baseline data and make small trim adjustments to coolant flow or feed preheat. Over time, these tweaks keep the bed closer to isothermal operation, extending catalyst life and improving product consistency.
Material Choices for Long-Lasting Infrared Emitters
For infrared emitters that need to survive tens of thousands of thermal cycles, the pairing of heating element and ceramic base is often the first failure point. Alumina is a common choice because its expansion coefficient sits close enough to nichrome and Kanthal wires to prevent stress fractures during ramp-up and cool-down. Where frequent on-off cycling is expected, zirconia-toughened alumina adds crack resistance but reduces thermal shock tolerance slightly, so the duty cycle matters more than the material spec sheet suggests.
Surface condition often determines longevity more than bulk chemistry. A bare refractory metal like tungsten or molybdenum radiates poorly and oxidizes quickly at high temperature unless a protective oxide or ceramic coating is applied. A thin layer of chromium oxide on Kanthal, or a plasma-sprayed alumina layer on Inconel, pushes emissivity from roughly 0.25 to above 0.8 while forming a self-healing barrier against further attack. The coating's adhesion under thermal expansion is what separates emitters that last five years from those that fail in five months.
For the harshest environments, silicon carbide elements remain a benchmark because the silica scale that forms on the surface is stable and slows further oxidation. But operators must account for the element's rising resistance over time, which requires a power supply that can adjust voltage upward. Tungsten halogen emitters offer a different path: the halogen cycle redeposits tungsten onto the filament rather than letting it coat the bulb wall, but only if the quartz envelope stays above about 250°C. That narrow window forces designers to choose housing materials that can tolerate both the temperature and trace halogen gases without corroding.
Field Data: Energy Use Patterns in Specialty Chemical Plants
Meter-level records from specialty chemical sites show that energy demand tracks production mode more closely than overall output. Batch reactors often spike during heat-up and cool-down phases, while separation columns and solvent recovery units can account for over half of total steam use in a given week. Product changeovers amplify this variability, pushing utilities well above average baselines for short intervals.
Field readings also expose a sizeable standby load when lines are idle. Compressed air, chilled water, and nitrogen purge systems keep running at partial capacity between campaigns, and in several plants these house loads represented roughly a third of non-production energy draw. Cleaning and drying steps tied to high-purity grades added further peaks that were rarely captured in design-stage estimates.
Comparing actual consumption against process design values shows gaps of fifteen to thirty percent in energy intensity. Much of this stems from off-design operation of pumps, fans, and heat exchangers when reactors run at reduced volume or under frequent thermal cycling. Operators that shifted energy-hungry separation tasks away from peak tariff hours reduced monthly power costs without altering total energy use, a pattern seen consistently in three mid-sized sites studied over an eighteen-month window.
Engineering Support from Pilot Scale to Full Production
Scaling a process from pilot runs to full production rarely follows a straight line. Small-batch successes often hide issues that only surface under continuous operation, higher throughput, or tighter cost targets. Engineering support at this stage means more than handing over a recipe; it involves re-evaluating heat transfer, mixing dynamics, and material handling at every step. A pump that worked fine for a 50-liter batch can cavitate at 5,000 liters, and a filtration setup that took an hour in the pilot plant might clog in minutes on the factory floor. Good engineering support translates those pilot learnings into robust, repeatable unit operations without assuming that “bigger” simply means “more of the same.”
One of the most overlooked parts of this transition is instrument placement and control logic. In a pilot setting, operators can manually adjust temperatures or feed rates based on visual cues. At full scale, those cues vanish behind closed vessels and automated sequences. Engineering support needs to identify which process variables truly drive quality and then build sensor networks and control loops around them, not around what was easiest to measure in the lab. This often means retrofitting existing equipment with additional probes, rewriting batch records to reflect realistic ramp times, and running deliberate stress tests to find where the process window actually closes. The goal is not to replicate the pilot run exactly, but to define a control space that delivers the same product attributes with far less human intervention.
Finally, full production brings a different set of constraints around raw material variability, equipment wear, and maintenance scheduling. Engineering support should anticipate these by designing in tolerance: specifying feed quality ranges that still hit spec, building cleaning cycles that prevent fouling between batches, and documenting what to do when a valve sticks or a steam trap fails. It also means training production staff not just to follow the procedure, but to understand why each limit exists. A process that survives the jump from pilot to full scale is rarely the one with the highest yield on paper; it is the one that keeps running when the plant is hot, the shift is long, and the next batch is already waiting.
FAQ
The core difference lies in how energy transfers. Far infrared panels emit wavelengths that penetrate directly into the reaction mass rather than warming the vessel wall first. This reduces thermal lag, shortens heat-up cycles, and prevents hot spots on the reactor surface. Many operators notice less scorching or product degradation because the heat distribution stays uniform across the full charge.
They pair each reactor with multi-zone controllers and tuned PID algorithms that respond to real-time sensor feedback. The heating elements are arranged in segmented arrays, so output can be scaled up or down without overshooting the setpoint. Even when switching between small pilot batches and full production volumes, the control logic adjusts ramp rates automatically.
Common users include specialty chemical plants, polymer synthesis labs, pharmaceutical intermediates, and food-grade extraction facilities. Because far infrared is gentle and non-contact, it suits heat-sensitive materials where conventional heating would cause localized overheating. Pilot-scale and continuous processing setups also integrate these reactors without major layout changes.
Yes, the manufacturer builds heating jackets and modules around the actual vessel geometry. Instead of forcing a standard size, they measure the reactor dimensions and split the heating surface into removable panels. This works well for retrofitting existing tanks or designing compact skids where clearance is tight.
The heating panels are designed for long service life with sealed ceramic or quartz elements, so routine upkeep is mostly inspection and cleaning. Controllers have self-diagnostic functions that flag drifting sensors or reduced output. The manufacturer also offers calibration support and stocks replacement modules that can be swapped without draining the reactor.
Because infrared transfers heat directly to the product, less energy is lost to air or metal surfaces around the vessel. Faster heat-up and cool-down cycles also reduce idle time between batches. Many facilities report lower kilowatt-hour consumption per kilogram of processed material after switching from jacketed oil or steam systems.
Each unit includes over-temperature cutoffs, ground-fault protection, and thermal fuses on the heating circuits. Panel surfaces are insulated to keep external temperatures low enough for safe operator contact. For hazardous areas, the manufacturer offers ATEX-rated enclosures and purged control cabinets that meet relevant classification requirements.
They run a factory acceptance test using a simulated load that mimics the customer's material properties. Temperature mapping verifies uniformity across the heating zone, and the control system is cycled through multiple setpoint changes. The test report travels with the unit, so the on-site team knows exactly what to expect during commissioning.
Conclusion
A far infrared heating reactor manufacturer delivers precision thermal solutions by embedding control logic and emitter placement directly into reactor design, rather than relying on blanket heating that struggles with tight temperature windows. Custom heating jackets are engineered to fit existing process lines, so plants can upgrade without cutting into vessels or reworking piping. The approach targets thermal gradients across catalytic beds, using segmented emitter zones and real-time feedback to flatten temperature differences that otherwise cause hot spots, uneven conversion, and premature catalyst deactivation. Material choices for the infrared emitters reflect the operating environment: quartz for clean high-temperature service, silicon carbide for aggressive atmospheres, and specialty alloys where mechanical stress is a concern. This selection extends emitter life and reduces maintenance shutdowns.
Field data from specialty chemical plants shows far infrared systems shifting energy use patterns in measurable ways. Instead of keeping large volumes of heat transfer fluid hot, these reactors deliver energy directly to the reaction mass, which lowers baseline demand and shortens heat-up cycles between batches. One pattern in the data is a drop in overnight idle load, since emitter banks can be modulated quickly without losing thermal stability. Engineering support bridges the gap between pilot-scale trials and full production, with teams adjusting emitter density, zone mapping, and control parameters as vessel geometry changes. That continuity preserves the thermal profile proven in the lab, so full-scale units reach yield targets sooner and with fewer commissioning surprises.
Contact Us
Contact Person: Mr. Wang
Email: [email protected]
Tel/WhatsApp: 8613705299955
Website: https://vip.e-baixing.com/szhgyw