In Line Shuttle Machine Solutions: Streamline Your Production Line with Precision Automation
2026-11-02
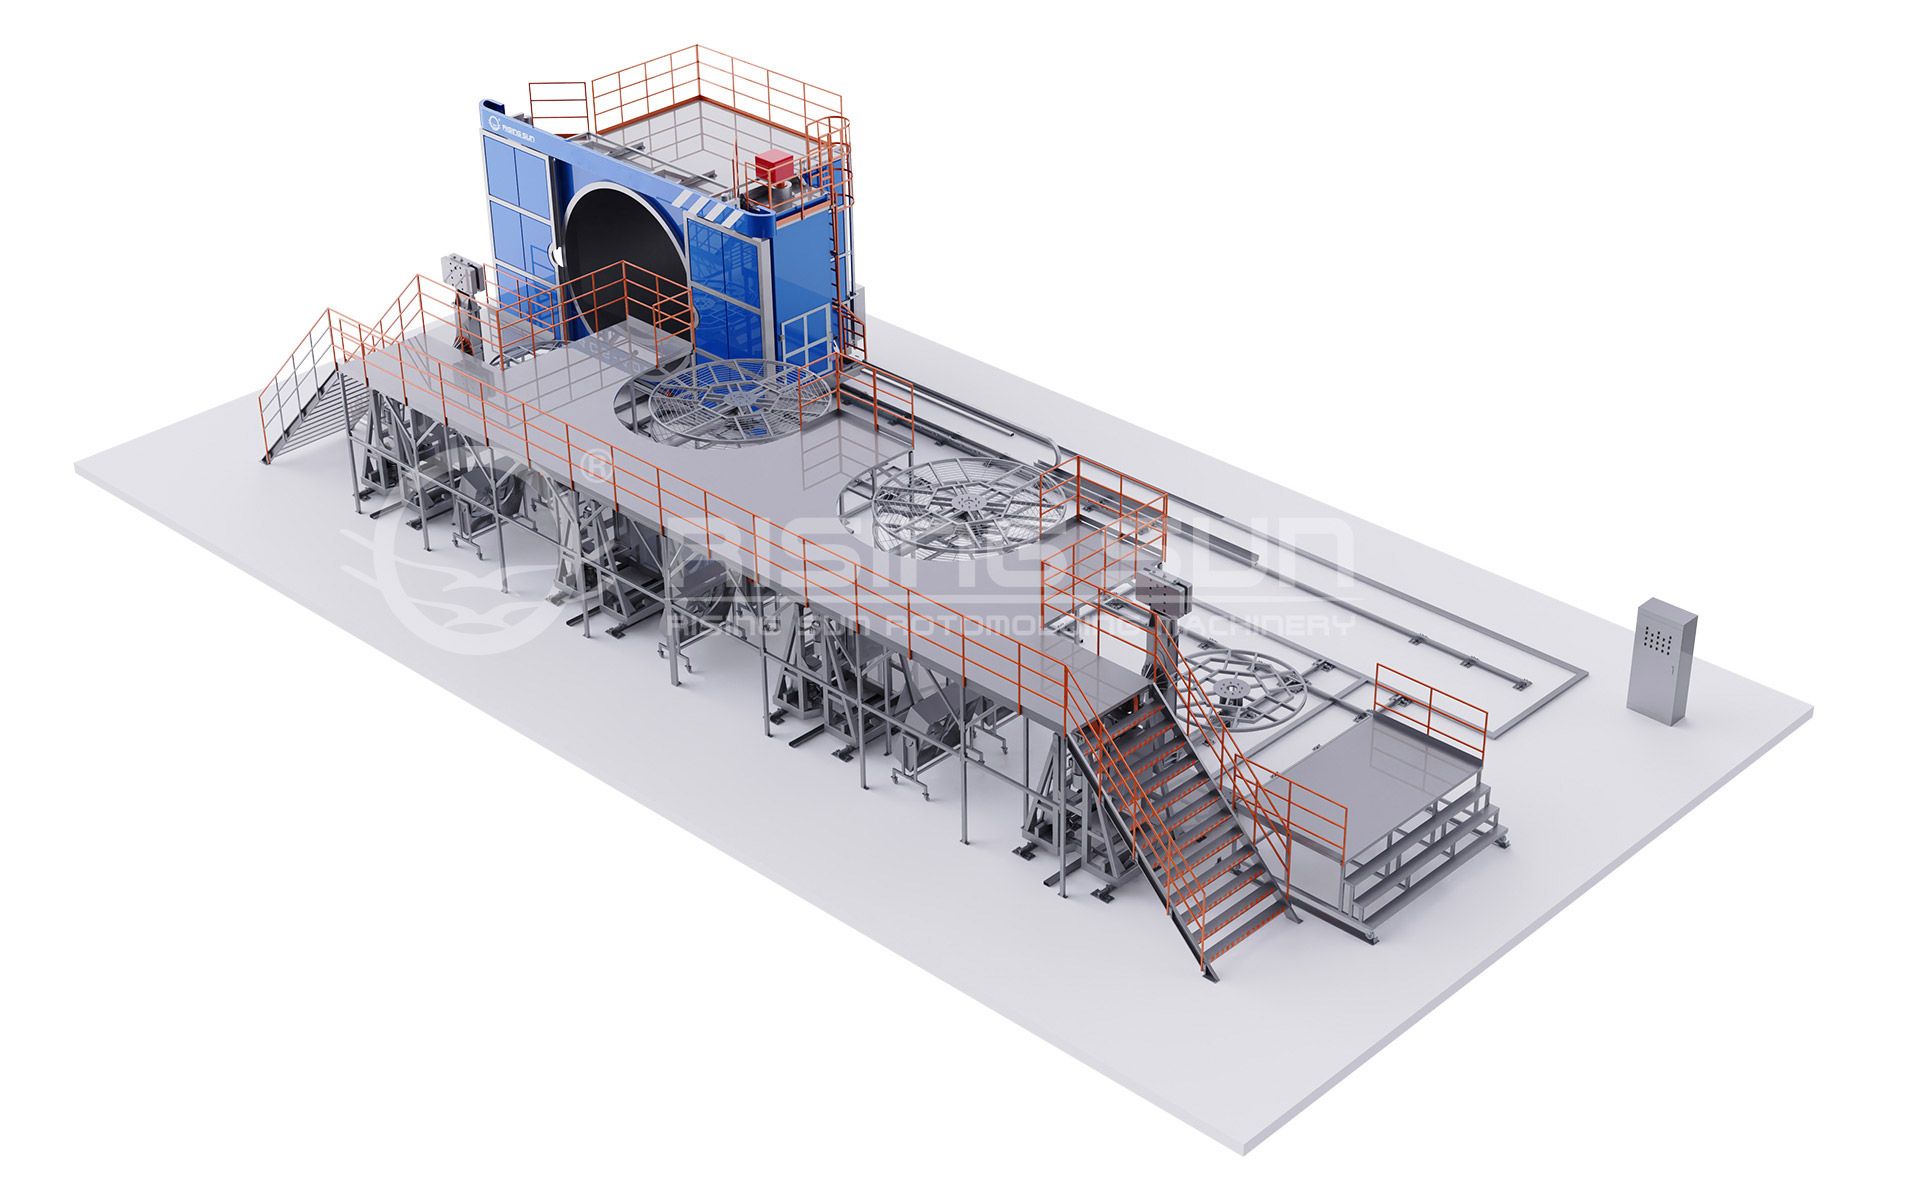
Precision automation often fails at the handoff—the moment a part leaves one station and enters the next. In-line shuttle machine solutions close that gap by synchronizing movement down to fractions of a second and microns of distance. At Rising Sun, we've seen how this one change can flatten bottlenecks and unlock hidden capacity. But not all shuttle systems are built the same, and the difference is rarely obvious until you look closely.
Precision That Keeps Your Line Moving
Precision here isn’t about hitting a spec sheet number once. It’s about every sensor reading, every actuator move, and every alignment staying within a tolerance band narrow enough that the next station never has to wait or compensate. When cut lengths repeat to the millimetre and placement drift stays negligible, the line keeps its rhythm without those quiet pauses that eat into daily output.
The real cost of imprecision rarely shows up as a dramatic breakdown. It hides in the small corrections operators make by hand, in occasional rejects that have to be pulled aside, in the gradual slowdown of a conveyor as someone double-checks a gap. Tight, repeatable motion removes that background friction, letting the line run at its intended pace for longer stretches.
That kind of consistency comes from design choices made early: bearings sized for the load, feedback loops that don’t chase their own noise, materials that resist wear instead of just surviving it. The result is a line that doesn’t demand constant attention, and that’s the precision people actually feel on the floor.
Cutting the Wait Between Stations
The minutes spent on a platform often feel longer than they actually are. Reducing the gap between trains or buses isn't just about adding more vehicles—it's about smarter dispatching, better coordination at transfer points, and responsive adjustments when delays occur. Small changes in headway management can ripple through the entire network.
Some systems now use live passenger counts and automatic vehicle location to fine-tune departure times instead of relying on fixed schedules. This means a slightly delayed bus can be held for a few seconds to let connecting riders board, while a train ahead of schedule might wait to even out spacing. The result is less bunching and fewer long, unexplained gaps.
Infrastructure also plays a role. Upgraded signaling, dedicated lanes, and platform design that speeds up boarding all contribute to shorter waits. When these pieces work together, a commuter’s experience shifts from watching the clock to simply catching the next ride.
Shuttle Paths That Fit Your Floor, Not the Other Way Around
Most shuttle systems make you bend your layout to their tracks. Our approach flips that. Instead of forcing your team to walk extra steps or rework storage zones, the path gets drawn around the exact shape of your floor. Columns, loading docks, narrow aisles—none of it becomes an obstacle. You hand us the blueprint, and the route simply follows the natural flow of how your people already move.
That means fewer compromises during installation. There’s no need to knock out a wall or sacrifice a staging area just to squeeze in a fixed loop. The shuttle’s guidance can hug tight corners, shift between floor levels, or even split off to a side lane when demand spikes in one section. The result is a setup that feels like it was always there, working quietly in the background.
What really changes is day-to-day operation. When the path mirrors your real workflow, operators spend less time waiting at transfer points or walking around machinery. Replenishment cycles shorten because the shuttle isn’t taking a scenic detour. And if your floor changes next year—a new rack line here, a pack station moved there—you just redraw the route. No new track, no major retrofit. Your floor stays in charge.
Handling Heavy or Fragile Payloads Without the Drama
Moving something delicate or absurdly heavy usually turns into a tense standoff between you, the object, and the floor. Instead of wrestling with guesswork, shift the focus to leverage and load distribution before you even lift. Slide a sturdy board under a fragile piece to create a stable base, or use rolling dollies with soft padding that grip without scratching. The goal isn't brute force—it's reducing the number of times the item needs to leave the ground, and making each lift as predictable as possible.
For awkward shapes or items with fragile corners, rigid supports beat soft wraps every time. Foam and blankets can hide pressure points, but they don't stop an item from flexing or cracking when tilted. Cut plywood braces to match the contour of the object, then strap them lightly—not tight enough to bite, just enough to stay put. If you're moving through doorways or tight turns, mark the floor path with low-tack tape first so you're not micro-adjusting while holding the load. Small pauses to realign your grip beat big last-second corrections.
Communication matters more than muscle when two people carry something fragile. Pick a single person to call the pace and direction, and stick to short, physical cues like “tilting toward you” or “setting down in three steps.” Avoid shouting “careful”—it adds tension without information. If the payload starts to shift, lower it onto a pre-placed block or cushion rather than trying to catch it mid-air. The drama disappears when every step has a fallback position, and you've already decided where the load will rest if your grip slips.
Smart Controls That Adjust on the Fly
You step into the room and the lights brighten before your hand reaches the switch. That's not a party trick—it's the baseline for smart controls that tune themselves to your habits and the current conditions.
Sensors pick up shifts in occupancy, daylight, temperature, even air quality. A meeting that runs long won't turn the room stuffy because the ventilation ramps up on its own. The thermostat doesn't wait for you to notice the chill; it nudges the heat when the outside temperature dips.
What makes it feel natural is that nothing demands your attention. No confirmation pop-ups, no manual overrides needed. The system reads the moment and adjusts quietly, so your space always feels just right without you having to think about it.
The End of Bottleneck Workarounds
For years, teams have refined the art of the workaround—juggling multiple tools, stitching together fragile scripts, and scheduling tasks around system slowdowns. But those days are fading. The fundamental shift is not a faster patch or a smarter queue; it's the removal of the bottleneck itself. When capacity, latency, and access no longer collide at a single choke point, the entire concept of a workaround becomes obsolete.
Consider how drastically priorities change once throughput is no longer constrained by a legacy gateway. Engineers stop asking “how do we route around this?” and start asking “what should we build next?” Instead of maintaining a parallel set of hacks to keep production moving, teams invest that energy directly into product logic and user experience. The result is not just a faster pipeline, but a cleaner mental model—one where exceptions are rare and the default path is always the right one.
This is not about making bottlenecks more tolerable; it's about rendering the entire category irrelevant. When the underlying architecture is designed so that no single component can throttle the rest, the vocabulary changes. You stop talking about fallback plans, retry storms, and degraded modes. The end of bottleneck workarounds means the end of compensating for a design that should never have existed in the first place. The freedom is subtle at first, then unmistakable: you simply do the work, and the system keeps up.
FAQ
Unlike a conveyor that just moves parts at a fixed pace, a shuttle uses linear servo or belt-driven carriages to position each workpiece with repeatable accuracy. That means you can stop at multiple assembly stations, index to a precise location, and run mixed models on the same line without re-tooling.
Yes, and that's often the fastest way to adopt it. Shuttles can deliver parts to a manual operator, wait for a cycle-start signal, then move on. The operator keeps flexibility while the automation handles transport and positioning, so you avoid large layout changes.
Typical systems hold location tolerances within ±0.05 mm using encoder feedback and rigid rail design. That's enough for press-fit, dispensing, screw driving, or vision-guided inspection without adding separate fixtures at every station.
They store recipes for each variant, so the shuttle position, speed, and station dwell time adjust automatically. Quick-change pallets or modular nests let operators swap over a family of parts in a few minutes, rather than rebuilding a dedicated line.
Labor is part of it, but often the bigger wins are reduced scrap from misaligned parts, higher throughput from parallel processing, and less floor space used by interim buffers. Many users see payback in under two years just from quality and throughput improvements.
Ask for references from lines with similar cycle times and part sizes. A good supplier will run a full risk assessment on your product geometry, provide simulation data for throughput, and offer remote diagnostics. Avoid vendors who only quote hardware without asking about your upstream and downstream processes.
They've become practical for medium batch sizes because the shuttles themselves are reusable. If you have a product family that changes a few times per shift, you can load a new fixture and call up a new program in less time than a traditional fixed automation line takes to rebalance.
Expect to inspect and lubricate linear guides every 500 hours, check belt tension if belt-driven, and recalibrate the home position after any crash or major changeover. Most of the electronics are sealed, so the main failures come from cable carriers and operators not keeping the rail area clean.
Conclusion
In line shuttle machine solutions rethink how materials move between assembly steps, replacing rigid conveyors and manual carts with a system that responds to actual production demands. The core advantage is precision without hesitation: shuttle carriers lock into position at each station within tight tolerances, so robots and operators can perform their tasks without waiting for alignment corrections. This accuracy cuts the wait between stations dramatically, because a shuttle can depart as soon as a cycle completes and arrive ready for the next step, not dwell in a buffer zone. The physical layout also adapts to you, not the other way around. Shuttle paths can curve, split, merge, or run along existing floor constraints, so there is no need to rearrange your entire plant just to fit automation. For payloads that are heavy, oddly shaped, or fragile, the motion profiles can be tuned to avoid jarring stops or sudden acceleration, keeping parts stable from pick to place.
What really removes the usual friction is the control layer. Instead of pre-programmed sequences that break down when a station slows or a part variant changes, smart controls monitor each shuttle's location, load status, and downstream congestion in real time. If a station needs extra seconds for a difficult assembly, the system adjusts spacing and speeds on the fly, preventing pile-ups and starvation. This dynamic response means you stop designing workarounds for bottlenecks, because the shuttle network routes around slow points or reorders tasks without manual intervention. Operators get a clear view of what is moving and why, but they do not have to chase the line or shuffle parts by hand. The result is a production flow that stays balanced even when product mix shifts, labor is reassigned, or an unexpected downtime event occurs upstream. In practice, that translates to more consistent output, less floor clutter, and a line that can scale without being torn apart and rebuilt.
Contact Us
Contact Person: Sharon Zhu
Email: [email protected]
Tel/WhatsApp: 8615712666272
Website: https://www.risingsunroto.com