OEM Steel Pipe Tower Dealers That Deliver Quality and Durability
2026-10-26
Finding OEM steel pipe tower dealers who actually deliver both quality and long-term durability is harder than it should be. Too many suppliers cut corners on steel grade or welding, leaving buyers with structures that age prematurely. That's exactly where Anbang comes in—a manufacturer that treats every tower as a long-term investment, not just a one-off order. In this post, we'll break down the key factors that separate reliable tower dealers from the rest and show why Anbang has earned a reputation for standing the test of time.
Checking Mill Certificates Before a Single Cut
A mill certificate is more than a bundle of paperwork—it's the only real link between the steel on your rack and the heat it came from. Before programming a single part, I spread the certs out next to the cut list and match each plate or beam back to its heat number. If the grade doesn't line up, or the yield strength is lower than what the job assumed, the cut hasn't happened yet, and that's exactly when the mistake is cheap to fix.
Traceability matters most when the part is buried inside a weldment or hidden behind a wall. Once the pieces are cut and mixed into a larger assembly, the heat number doesn't magically reappear. I've learned to record the cert number directly on the nesting layout and keep a photo of the physical marking before the first torch fires. It takes an extra minute, but it saves hours of arguing later if a test coupon fails or an inspector asks for backup.
The habit also catches supplier mix-ups that never show on a visual check. Two plates can look identical and still carry different carbon equivalents, different impact ratings, or different countries of origin. When the certs are reviewed line by line—not just skimmed for a grade—the wrong material stays on the rack. That discipline before the first cut is what keeps a shop from turning good stock into expensive scrap.
Wall Thickness Rules for Long Tapered Sections
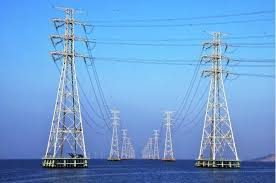
For elongated tapered forms, the biggest risk isn't the thin end itself but the rate at which the wall loses thickness over distance. If the section narrows too quickly, the material can't redistribute stress smoothly, and you'll often see localized buckling or a visible sink mark near the transition. A practical starting point is to keep the taper angle below roughly three degrees unless the part has added ribs or gussets to stabilize the long faces.
Wall stock should also follow a gradual gradient rather than stepping down in abrupt increments. Sudden drops in cross-section act like hinges, concentrating flex where the thickness changes. For parts longer than about six times their average diameter, consider breaking the taper into two or three blended zones, each with its own draft and thickness floor. This prevents the mid-span from becoming too flexible while still allowing the tip to fill cleanly.
Finally, check the ratio of wall thickness to overall length. Even a well-tapered section can become unstable if the thin end drops below 40 percent of the thick end over a short span. When the ratio is tighter than that, adding a shallow center rib or slightly increasing the base wall often performs better than trying to fine-tune the taper alone. In practice, the most reliable parts keep the thickest wall at the gate or feed end and let the taper work with the flow direction, not against it.
Why Galvanizing Alone Misses the Mark in Coastal Zones
Coastal environments punish steel in ways inland settings rarely do. The salt-laden air, high humidity, and constant wet-dry cycles create an electrochemical playground where zinc coatings erode far faster than design life calculations suggest. Galvanizing relies on sacrificial protection, but in marine atmospheres the zinc layer often thins unevenly, exposing bare steel at edges, welds, and abrasion points long before the coating reaches its nominal service life. Within months, rust blooms appear where the galvanic layer has been locally depleted, undermining the entire protective system.
The problem lies not just in corrosion rates but in the geometry of coastal structures. Bolted connections, drainage channels, and shadowed crevices trap chloride-bearing moisture, creating microclimates where the pH drops and the zinc's passive film breaks down. Galvanizing alone cannot bridge these hidden corrosion fronts; once the underlying steel is exposed, the remaining zinc accelerates attack in those spots through galvanic coupling. Repainting over active rust in such zones often fails within a season, leading to repeated maintenance cycles that cost far more than a properly selected duplex system from the start.
Specifiers who rely solely on hot-dip galvanizing for coastal projects frequently overlook the mechanical damage that occurs during transport, installation, and routine service. Crane hooks, bolt torquing, and wave-driven debris scrape off zinc in localized patches. Without a compatible topcoat to restore barrier protection, these scratches become initiation points for rapid pitting in chloride-rich air. The true lesson from decades of coastal failures is that galvanizing provides a strong foundation, but only a matched organic coating system can seal the inevitable breaches and keep the steel substrate isolated from the aggressive marine environment.
Custom Pole Profiles Without Long Lead Times
Getting a pole profile tailored to your exact specifications no longer means waiting months for tooling or shipping. Many manufacturers now keep a range of base profiles in stock and use in-house bending, punching, and welding stations to adapt them within days. This approach lets you request specific wall thicknesses, slot patterns, or mounting hole placements without triggering a complete custom production run.
What shortens the timeline is the shift from hard tooling to modular forming and CNC-driven fabrication. Instead of cutting new dies for every variation, shops can program a machine to produce small batches of unique profiles from standard blanks. As a result, even one-off prototypes or limited project runs can be ready in a couple of weeks rather than a full quarter.
The real advantage shows up on job sites that need odd lengths, non-standard diameters, or special alloy finishes. You get the exact geometry and performance you specified, without paying a premium in time. If your project has a tight deadline, ask suppliers about their quick-change tooling and stocked pre-forms—these are often the reason a custom pole profile can ship almost as fast as a standard one.
Load Tests That Match the Wind, Not Just the Spec Sheet
Engineers often treat load testing as a box-ticking exercise: run the numbers from a datasheet, apply a safety factor, and call it a day. But real-world structures don't experience neat, uniform pressures. Wind gusts, turbulence, and local terrain effects create wildly uneven loading that no static spec sheet can capture. A more honest approach starts by asking what the wind is actually doing at the site—not just what the code says it might do.
That means looking beyond basic velocity pressure and instead mapping the full dynamic signature of the wind. Buffeting, vortex shedding, and wake effects from nearby buildings or hills can impose fatigue cycles that far exceed the simple maximum load. We've seen towers pass a conventional static test, then develop cracks within two years because the test ignored the repeated, low-amplitude stress reversals caused by wind direction switching. A load test that matters replicates those patterns, not just a single peak gust.
The practical takeaway is to instrument structures with enough spatial resolution to catch local pressure spikes. Rooftop corners, parapets, and cladding attachment points often see two to three times the average pressure. If your load test only validates the mid-span moment, you're leaving the most vulnerable spots untested. Field measurements from anemometers and pressure taps, fed back into the test sequence, turn a generic protocol into something that mirrors the site's actual wind behavior. That's the difference between a structure that passes on paper and one that survives a decade of storms.
Installation Support That Continues After the Truck Leaves
Most suppliers consider the job done once the delivery truck pulls away. We take a different view. Every unit ships with a dedicated installation kit that includes torque specs, alignment guides, and a short video walkthrough recorded for your exact configuration. If questions come up mid-install, a direct line connects you to the engineer who signed off on your order—not a generic call center.
That line stays open after startup. Within the first week, we schedule a 20-minute follow-up call to walk through mounting stability, wiring connections, and any unusual vibrations. For teams that prefer hands-on help, our regional field technicians can stop by without a service contract. They carry spare fasteners, shims, and calibration tools so minor adjustments don't turn into downtime.
Long-term support is just as practical. If a component wears or a new operator takes over, we can ship replacement parts with step-by-step photos or re-shoot a training clip for the new setup. You're not left sorting through a PDF manual—you get answers that match the equipment sitting in your facility right now.
FAQ
Look beyond the price tag and inspect the raw material sourcing, welding consistency, and coating thickness. A dealer that openly shares mill certificates and allows third-party inspection tends to be more dependable.
Check the galvanization layer and ask about wind load calculations for your specific region. Real durability comes from proper base plate design and corrosion-resistant fasteners, not just thicker pipe walls.
OEM dealers have direct influence over the production line, so adjustments to flange spacing, ladder placement, or mounting brackets happen without awkward compromises. That control reduces field modifications later.
Expect changes in tower height, pipe diameter, joint styles, and accessory mounting points. A quality dealer will also adjust the design to match local soil conditions and antenna loading requirements.
Telecom companies, broadcast stations, utility providers, and security system integrators rely on OEM steel pipe towers for monopoles, camera mounts, and transmission structures where stability is critical.
Watch for vague answers about steel grade, unusually short lead times without explanation, or reluctance to provide sample sections. Also avoid dealers that mix scrap metal into the pipe batch to lower cost.
Established dealers usually commit to realistic windows based on current steel market conditions and factory capacity. They also coordinate flatbed transport with proper load securing, reducing damage before the tower reaches your site.
Conclusion
Quality in steel pipe towers starts long before welding begins. A reputable OEM dealer will pull mill certificates for every heat of plate and coil, verifying chemistry and tensile strength instead of trusting a supplier's word. For long tapered sections, wall thickness isn't a single number; dealers who understand bending stress specify step-down transitions and tolerances that hold across the entire length. In coastal zones, hot-dip galvanizing alone is rarely enough—smart dealers pair it with duplex coatings or zinc-rich primers to fight salt spray and premature rust at bolted joints.
Custom pole profiles don't have to mean months of waiting when the dealer keeps standard plate widths and forming dies ready to adjust rather than starting from scratch. Wind load tests should replicate actual gust patterns and fatigue cycles from the site, not just a generic spec sheet. Even after delivery, installation support matters: bolt torque guidance, foundation checks, and field touch-up advice continue after the truck leaves the yard. That combination of material traceability, honest engineering, and post-sale follow-through is what separates true OEM partners from order takers.
Contact Us
Contact Person: antor khan
Email: [email protected]
Tel/WhatsApp: 8613863903569
Website: https://www.qdabtower.com/