Shank Adapter Factories: Top 10 Manufacturers for Durable Tooling
2026-09-29
Finding a shank adapter factory that won’t let you down mid-project is harder than it sounds. Too many suppliers promise durability but deliver early wear, poor heat treatment, or threads that strip under load. That’s exactly why we put together this list of the top 10 manufacturers—including PULANKA—so you can skip the trial and error and go straight to tooling that holds up. From material selection to real-world performance, here’s what sets the best apart.
Why the Melt Shop Decides Shank Adapter Lifespan
The melt shop sets the stage for shank adapter longevity long before the first strike. Chemical composition, inclusion content, and solidification structure all originate in the furnace and ladle. A steel with high purity and controlled residual elements resists crack initiation under cyclic impact, while a coarse or segregated as-cast grain pattern from poor melting practice can seed fatigue failures that no heat treatment can fully erase.
Cleanliness is not just a buzzword here—it directly translates into how many meters a shank adapter drills before snapping. Non-metallic inclusions like alumina or silicate clusters act as stress concentrators. When the melt shop uses proper deoxidation, vacuum degassing, or argon rinsing, inclusion counts drop and the adapters show a markedly longer service life. On the other hand, a melt with high oxygen or nitrogen levels produces brittle, unpredictable steel that fails early under percussion loads.
Even the casting method chosen by the melt shop matters. Continuous casting with tightly controlled cooling yields a fine, uniform dendritic structure, while ingot casting with insufficient hot topping can leave centerline porosity. Such porosity becomes a hidden defect that grows with every blow, eventually causing a sudden fracture. Thus, the fate of a shank adapter is often sealed not on the drill rig, but in the crucible where the first atoms solidify.
Heat Treatment Tricks That Cheap Factories Skip
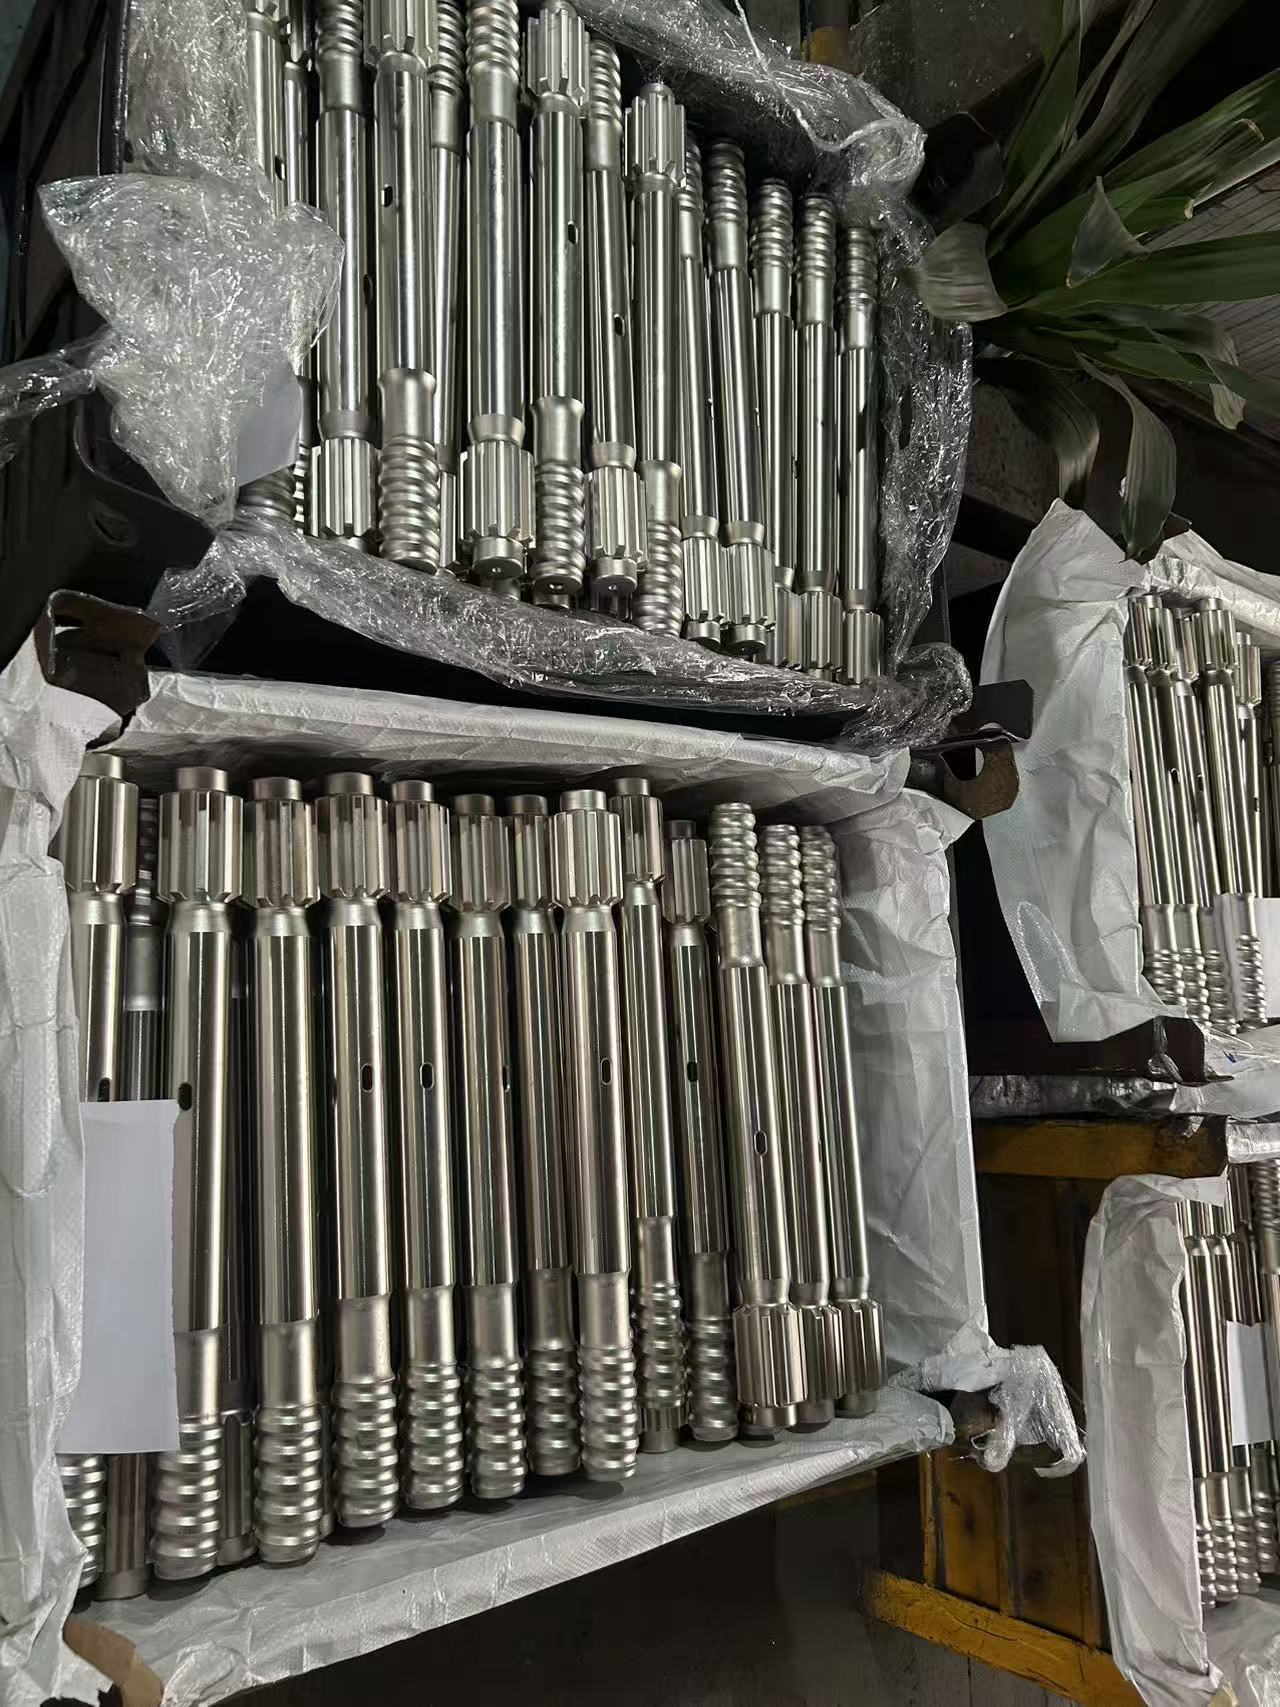
A lot of budget factories will harden a batch of blades or gears just long enough to pass a file test, then ship them out the door. What they skip is the long soak at temperature—sometimes 20 to 40 minutes beyond the surface reading—that lets the core actually transform. Without that hold, you end up with a hard skin over a soft center, and the part fails the first time it sees real torque or repeated impact.
Another trick that gets skipped is cryogenic treatment after quenching. It sounds exotic, but for high-alloy tool steels and stainless cutters, a controlled drop to around -100°F or lower converts retained austenite into fresh martensite. The result is a part that doesn't just measure hard, it stays dimensionally stable. Shops that skip this save a few hours and a little liquid nitrogen, but their knives and dies drift after sharpening or start chipping at the edge.
Then there's the tempering cycle. Cheap operations often do one quick temper, or none at all, because the part already "feels" hard. A proper shop will run two or even three tempers, each with a full cool-down to room temperature in between. This not only relieves quench stress but also evens out hardness across the entire batch. Skipping the second temper is invisible on a spec sheet, but it's exactly why some cheap tools snap where better ones flex.
Surface Finish as the Overlooked Wear Factor
In most wear analyses, hardness and lubrication dominate the conversation, while surface finish quietly sets the stage for everything that follows. A surface that looks smooth to the naked eye can still harbor microscopic peaks and valleys that act as initiation points for abrasion, adhesion, and fatigue. When two components slide or roll against each other, these tiny irregularities concentrate contact stresses far beyond what the bulk material would suggest, accelerating material removal long before any obvious damage appears.
The paradox is that overly polished surfaces are not always the answer. A mirror-like finish can reduce oil retention, leading to boundary lubrication breakdown and increased metal-to-metal contact. Conversely, a deliberately textured surface—engineered with controlled roughness orientation and depth—can trap debris, distribute load more evenly, and even create hydrodynamic lift that separates mating parts. The key lies not in chasing the lowest Ra value, but in matching the finish pattern and amplitude to the specific wear mechanism at play.
Field failures often reveal the true cost of ignoring this factor. Bearings that pass hardness and clearance checks still fail prematurely because the shaft was ground with a random crosshatch angle that pumped lubricant out instead of in. Gear teeth with chatter marks from final machining create stress risers that lead to micropitting. No amount of premium lubricant can compensate for a surface topography that works against the tribological system. Until designers treat surface finish as a deliberate design parameter—not a leftover from manufacturing—wear prediction will remain an exercise in educated guessing.
Beating Up Shank Adapters Before They Reach You
Every shank adapter that leaves our facility has already taken a beating. We don't just inspect them visually; we clamp them into test rigs and hammer them with impact loads that mimic worst-case jobsite abuse. Bent, twisted, and smacked against hardened steel, these adapters have to survive repeated blows before they earn a spot in the box.
Most failures happen at the connection point, so that's where we focus the punishment. We cycle the adapter through thousands of stress reversals, checking for hairline cracks that would only show up after weeks in the field. If a batch shows even one micro-fracture under dye penetrant, the entire run gets scrapped, not sorted.
By the time one reaches you, it's already been through more punishment than most job sites dish out in a year. That's intentional. A shank adapter shouldn't be the weak link in your tool string, and we'd rather break them here than have you find the limit on a Friday afternoon.
Made-to-Order Shanks for Unusual Drill Rigs
Not every drill rig rolls off a standard production line, and the shank that fits it rarely comes off a shelf either. When you're running an older crawler, a modified mast, or a one-off machine built for a narrow trenching job, the interface between hammer and drill string demands more than an off-the-shelf adapter. Made-to-order shanks are machined to match the exact spline count, shoulder diameter, and retention groove your rig needs—often reverse-engineered from a worn sample or a hand sketch.
The real difference shows up in material selection and heat treatment. We've produced shanks from 4340 and 4145H modified bar stock, through-hardened to handle the shock loads of a rig that was never meant to run a modern down-the-hole hammer. Threads get rolled or cut after heat treat only when the design calls for it, and every shank leaves with a dimension report tied to your rig's serial number.
Turnaround is usually two to three weeks, depending on whether we need to source unusual forgings or machine from solid. Send us the broken piece, a rubbing of the splines, or just a list of measurements—we'll work out the rest and ship a shank that drops in without field grinding.
Small Batch, Same Tough Standards
When we decided to keep production runs small, it wasn’t about cutting corners or chasing exclusivity. It was about making sure every single unit gets the attention it deserves. A smaller batch means fewer pieces pass through our hands each day, but each one still faces the same gauntlet of checks, measurements, and real-world tests that our largest orders do. There’s no “good enough for a short run” here—either it meets the full list of requirements, or it never leaves the workshop.
Every component that goes into a finished piece is inspected under magnification before assembly. Threads are checked for burrs, surfaces are gauntlet-tested against corrosion, and torque values are recorded for anything that moves. We keep a paper trail for each batch, down to the humidity in the room during final fitting. If a single spec drifts outside its tolerance, the whole run gets pulled apart and rebuilt—no exceptions, no shortcuts, and definitely no signing off on “close enough.”
The payoff is in the details you can feel. A knob that turns with the exact same resistance every time, a seam that stays invisible after months of use, a finish that doesn’t dull unevenly. Small batch doesn’t mean we relax the rules—it means we have fewer chances to hide behind averages. Every piece carries the weight of the whole standard, and that’s exactly how we want it.
FAQ
You will usually see names like Sandvik, Epiroc, Robit, and Boart Longyear come up in field reports, but smaller Swedish and Finnish workshops also build excellent adapters because they control heat treatment in-house. The real test is not the brand alone; ask for batch-level fatigue data and inspect how they handle carburizing depth.
They pay obsessive attention to the transition zones. A proper factory will use vacuum-degassed steel, machine the threads after heat treatment to avoid distortion, and often apply shot peening to the critical shoulder. Some also run ultrasonic inspection on every batch, not just samples.
Durability usually comes down to three things: the cleanliness of the steel, the precision of the thread profile, and whether the factory runs a controlled cooling curve after carburizing. Cheap plants skip the final grinding step, which leaves stress risers that crack after a few hundred blows.
Northern Europe gets most of the attention because of the mining equipment legacy, but Japan and South Korea have very disciplined machining cultures, and some Chinese factories have upgraded to European heat-treating lines. Turkey and India are also becoming interesting for mid-range adapters if you can verify the metallurgy.
Ask for a full material certificate, the exact heat treatment curve, hardness readings at several points, and a small pilot batch for field testing. If they hesitate to share any of that, keep looking. Also clarify whether they can hold tolerances on the thread runout, because that is where premature failures start.
Top hammer adapters are shorter and must transmit intense axial impacts through a threaded connection, so the thread root design and shoulder geometry matter most. DTH adapters work more as torque and air flow conduits, so the spline profile and sealing surfaces get the attention. A factory that understands both will not offer a one-size-fits-all design.
Vague answers about steel grade, a refusal to share heat treatment details, or a price that seems too good to be true are all red flags. Also watch for adapters that arrive with rough thread flanks or no traceability markings. Those small omissions usually mean the plant skipped steps you cannot see from the outside.
Conclusion
The real lifespan of a shank adapter starts in the melt shop, where alloy cleanliness and inclusion control quietly set the ceiling for fatigue resistance. Top-tier factories in the durable tooling space don't treat steel sourcing as an afterthought—tight limits on sulfur, phosphorus, and non-metallic inclusions mean fewer crack initiation sites down the road. From there, heat treatment separates serious producers from budget shops. The cheap route is a single quench and temper; the better route adds controlled normalizing, multi-stage tempering, and sometimes cryogenic treatment to stabilize retained austenite. Surface finish often gets overlooked, but tool marks and rough transition radii act as stress risers. The best manufacturers polish critical zones and specify edge breaks that extend service life under high-frequency hammering.
Before any adapter ships, the strong factories abuse their own products on impact test stands, cycling them through simulated rock drilling to catch microcracks and dimensional drift early. That pre-delivery punishment is rare among low-cost suppliers. When a drill rig has an odd shank length, non-standard spline, or custom shoulder, the leading names offer made-to-order work without treating it as a burden. Just as important, they hold the same hardness, straightness, and surface finish on a five-piece prototype as on a full production run. This blend of melt-shop discipline, unskipped heat treatment, honest fatigue testing, and small-batch rigor keeps a short list of shank adapter factories ahead of the field for durable tooling.
Contact Us
Contact Person: Elma
Email: [email protected]
Tel/WhatsApp: +86 13738628777
Website: https://www.pulankagroup.com/