Zinc Diethylphosphinate Exporter Factory: Reliable Supply and Quality Assurance
2026-08-11
When sourcing zinc diethylphosphinate for flame retardant applications, reliability and quality aren't just nice-to-haves—they're everything. But finding a supplier that consistently delivers both can feel like searching for a needle in a haystack. That's where X.X.F.R comes in. As a specialized exporter factory, we've built our reputation on unwavering supply stability and rigorous quality assurance, ensuring your production never misses a beat. In this post, we'll peel back the curtain on what makes a zinc diethylphosphinate supplier truly stand out—and why X.X.F.R might just be the partner you've been looking for.
Precision Manufacturing for Consistent Product Purity
Every component in our production line is calibrated with meticulous attention, ensuring that each batch meets exacting purity standards. By integrating advanced automation with real-time monitoring, we eliminate the variations that often compromise product quality. This disciplined approach turns precision from a goal into a guarantee, delivering results you can rely on time after time.
Our manufacturing environment is engineered to minimize contamination risks, from the handling of raw materials to the final packaging stage. Specialized filtration systems and controlled atmospheres work in concert to preserve the integrity of the product, while rigorous in-line testing catches any deviation before it ever reaches you. It’s a seamless fusion of technology and craftsmanship that keeps purity constant.
What sets this process apart is the feedback loop between our quality assurance teams and the production floor. Insights from purity analysis directly inform machine adjustments, fostering a culture of continuous refinement that static protocols simply cannot achieve. The result is a product whose purity isn’t just measured, but predictably sustained across every order.
Global Logistics Backed by Decades of Export Expertise
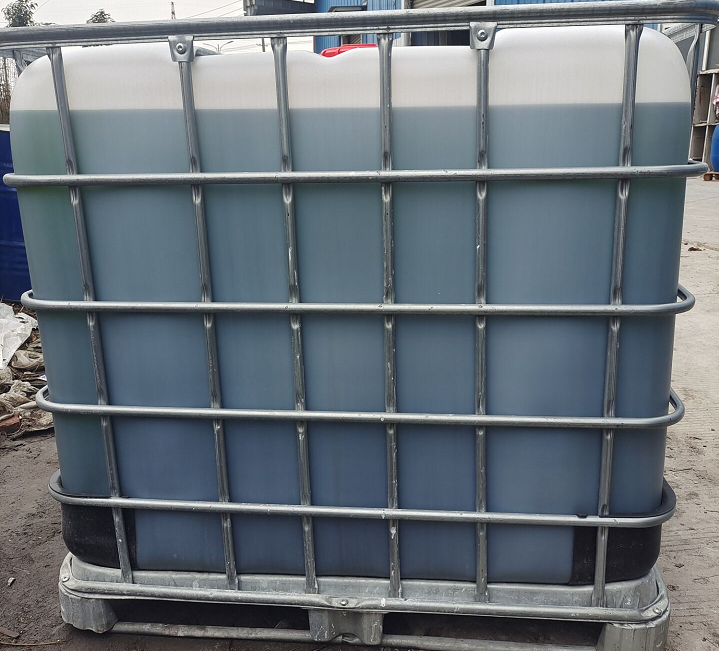
Understanding the intricacies of international shipping lanes, customs protocols, and local trade regulations doesn't come from books—it's earned through years of hands-on dispatch across every continent. Our team has navigated port strikes, shifting tariffs, and last-minute reroutes with a calm efficiency that only repeat exposure can build. That depth of experience means we anticipate snags before they derail a shipment, keeping your goods moving when others stall.
Real export expertise shows in the layers beyond transportation: harmonized code classification, accurate landed-cost estimation, and diplomatic handling of cross-border paperwork. We've cultivated direct relationships with freight forwarders, customs brokers, and overseas partners who treat your cargo with the same urgency we do. Because we know that a delayed shipment doesn't just eat into margins—it erodes trust with your buyers.
The result is a logistics framework that adapts to product-specific demands, whether you're sending perishables that need cold chain continuity or heavy machinery requiring special permits. Every link in the chain has been tested and refined across decades of exports, so you're not depending on generic workflows but on a proven system molded by real-world outcomes.
Rigorous Quality Checks From Raw Material to Final Shipment
Every component that enters our production line is scrutinized against a detailed checklist—no shortcuts, no assumptions. From alloy composition and dimensional tolerances to surface integrity, raw materials are verified with spectrometry, hardness testers, and coordinate measuring machines before they ever touch a workbench.
During assembly, in-line inspection stations monitor critical parameters at each stage. Our technicians use both automated vision systems and hands-on gauging to catch deviations early, ensuring that issues are fixed on the spot rather than passed down the line. This layered approach eliminates the blind spots that batch sampling can miss.
Final shipment isn’t just a formality—every outgoing unit undergoes functional testing that simulates real-world stresses, from thermal cycles to vibration. Only after passing this gauntlet, with detailed records attached to each serial number, does an order leave our dock. That way, we’re not just checking boxes; we’re guaranteeing performance you can count on.
Customized Formulations to Meet Diverse Industrial Needs
Industrial environments vary tremendously, each presenting its own set of performance requirements, material compatibilities, and operational conditions. Off-the-shelf chemical blends rarely address these nuances effectively, which is why tailored formulations have become essential. From extreme temperature resistance to specific viscosity profiles, customized solutions are engineered to integrate seamlessly into existing processes without forcing compromises on quality or efficiency.
Developing a bespoke blend involves close collaboration with technical teams to map out every critical parameter—whether it's the pH range for a cleaning agent, the curing speed of an adhesive, or the dielectric strength of a protective coating. This rigorous approach ensures that the final product not only meets but often exceeds the original specifications, offering a competitive edge in industries as varied as aerospace, electronics, and heavy machinery.
Beyond mere technical alignment, customized formulations also factor in sustainability targets and regulatory compliance, helping manufacturers stay ahead of evolving standards. By adjusting raw materials and reducing hazardous components without sacrificing performance, these solutions contribute to safer workplaces and a smaller environmental footprint. It's a partnership-driven model where each batch is a direct response to real-world challenges, not just a catalog item.
Sustainable Practices That Reduce Environmental Impact
Adopting circular design principles can dramatically cut waste before it even exists. Instead of the old “take-make-dispose” model, companies are rethinking products to be disassembled, repaired, or remanufactured. For instance, modular smartphones with replaceable parts extend device lifespans and reduce e-waste. This shift isn’t just about recycling—it’s about designing out waste from the start, which minimizes resource extraction and the energy burden of constant manufacturing.
Renewable energy integration is moving beyond simply installing solar panels on rooftops. Smart grids and localized microgrids let communities share surplus power, making clean energy more resilient and accessible. In urban areas, building materials like photovoltaic glass transform entire structures into power sources without sacrificing aesthetics. Pairing this with real-time consumption feedback helps households and businesses adjust usage patterns, slashing both carbon footprints and utility bills in tangible ways.
Regenerative agriculture goes a step further by actively healing ecosystems while producing food. Techniques like agroforestry, cover cropping, and holistic grazing rebuild soil health, sequester carbon, and improve water cycles. When local supply chains prioritize these methods, the environmental cost of transportation and refrigeration drops. It’s a quiet revolution that shows how our food systems can actually restore the planet instead of just sustaining its current state.
Dedicated Support Before, During, and After Your Order
From the moment you reach out, a real person takes time to understand what you’re trying to achieve—no scripted responses, just honest guidance. We help you navigate options, clarify details, and avoid the guesswork so you feel confident before you even place an order.
Once your order is in motion, you’re never left in the dark. Updates come directly from the team handling your request, not automated bots. If something shifts or a question pops up, we’re reachable and ready to adjust, keeping things on track without making you chase information.
Even after everything is delivered, the door stays open. Need a tweak, a revisit, or just a second pair of eyes? We stick around because good support doesn’t have an expiration date—it’s just part of how we work.
FAQ
It's a phosphorus-based flame retardant mainly added to engineering plastics like polyamides and polyesters. You'll find it in electrical connectors, automotive parts, and electronic housings where high heat resistance and electrical properties matter.
We run our own production lines and don't rely on middlemen, so pricing stays consistent and lead times are predictable. Plus, we've been exporting this specific chemical for over a decade, so we know how to handle everything from custom blends to last-minute orders.
We keep strategic buffer stocks of key intermediates and have backup suppliers under long-term agreements. Our plant also runs modular reactors, so we can shift capacity between products if one line faces a pinch.
Every batch goes through ICP for metal traces, HPLC for purity, and a thermal stability test that mimics processing conditions. We also retain samples for two years. If something looks off, we halt shipment and re-test before it leaves the gate.
Absolutely. We have in-house milling and coating capabilities. Just share your target D50 and any compatibility requirements—like silane treatment for better dispersion in nylon—and we'll run pilot batches for your approval.
Our zinc diethylphosphinate is REACH registered and RoHS compliant. We can also provide a full EN 45545-2 test report for rail applications, and we're ISO 9001 and 14001 certified at the factory level.
We prepare all documents in-house—MSDS, certificate of origin, packing list, bill of lading—and work with forwarders who specialize in hazmat chemicals. If your country has special import rules, we'll pre-file samples so there are no surprises at the port.
First, we'll send our application engineer to your site to look at your processing conditions. Often it's a temperature or compounding mismatch, not the additive itself. If the problem is genuinely ours, we replace the batch and cover the freight.
Conclusion
Operating as a specialized exporter of zinc diethylphosphinate, our factory places unwavering emphasis on precision manufacturing to ensure every batch meets exacting purity standards. From sourcing verified raw materials to employing advanced synthesis and refinement processes, we maintain consistent chemical and physical properties that our global clients can depend on. Decades of export experience have shaped a logistics framework capable of navigating complex international regulations, customs protocols, and varied climate conditions—guaranteeing on-time delivery without compromising product integrity. This operational maturity, combined with a deep understanding of regional market demands, enables us to offer customized formulations tailored to specific flame retardancy requirements, processing parameters, or compatibility needs across diverse industries such as electronics, automotive, and construction.
Quality assurance extends far beyond the production floor: it is embedded in every stage, from incoming material inspection to final shipment verification. Rigorous testing protocols—including spectroscopic, chromatographic, and thermal analyses—are conducted in our in-house laboratories to confirm compliance with international standards and client-specific thresholds. Equally vital is our commitment to sustainable practices; we have integrated closed-loop water systems, solvent recovery units, and waste minimization strategies to reduce environmental impact without sacrificing product performance. Throughout the entire journey, clients receive dedicated support—whether for technical consultation, order tracking, or post-delivery troubleshooting—fostering partnerships built on trust and long-term reliability. This holistic approach not only safeguards your supply chain but also aligns with responsible stewardship goals.
Contact Us
Contact Person: Guohua Wang
Email: [email protected]
Tel/WhatsApp: 8613003442895
Website: https://www.xxflameretard.com